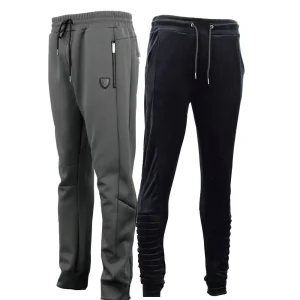
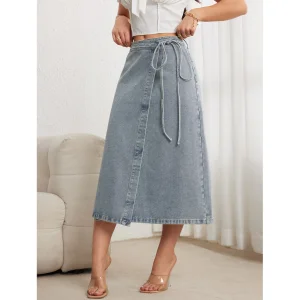
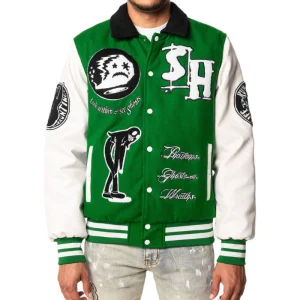
High-performance structural knits, heavy-weight utility garments, and precision-engineered casual wear ready for global supply chain distribution.
In the contemporary B2B apparel sector, selecting a premier long sleeve tees supplier and exporter goes far beyond superficial unit-cost comparisons. Corporate buyers, lifestyle fashion labels, and high-growth retail brands require deep technical capabilities, responsive agility, and uncompromised compliance structures. Long-sleeve garments present distinct manufacturing challenges relative to standard short-sleeve tees: sleeve draping alignment, cuff ribbing tension recovery, sleeve-to-shoulder seam durability, and multi-panel wash stabilization.
As market dynamics skew toward micro-trends and volatile consumer demands, the traditional multi-month development cycle has collapsed. Modern procurement directors look for vertical integration, raw-material buffer reserves, and sophisticated technological stacks. The following whitepaper details the modern benchmarks, material science frameworks, and structural supply chain advantages that define the top tier of international garment production.
The global textile value chain is currently operating under a complex matrix of shifting customs regimes, strict chemical usage codes, and carbon footprint reduction targets. A top-tier long sleeve tees exporter must demonstrate control across three primary operational axes:
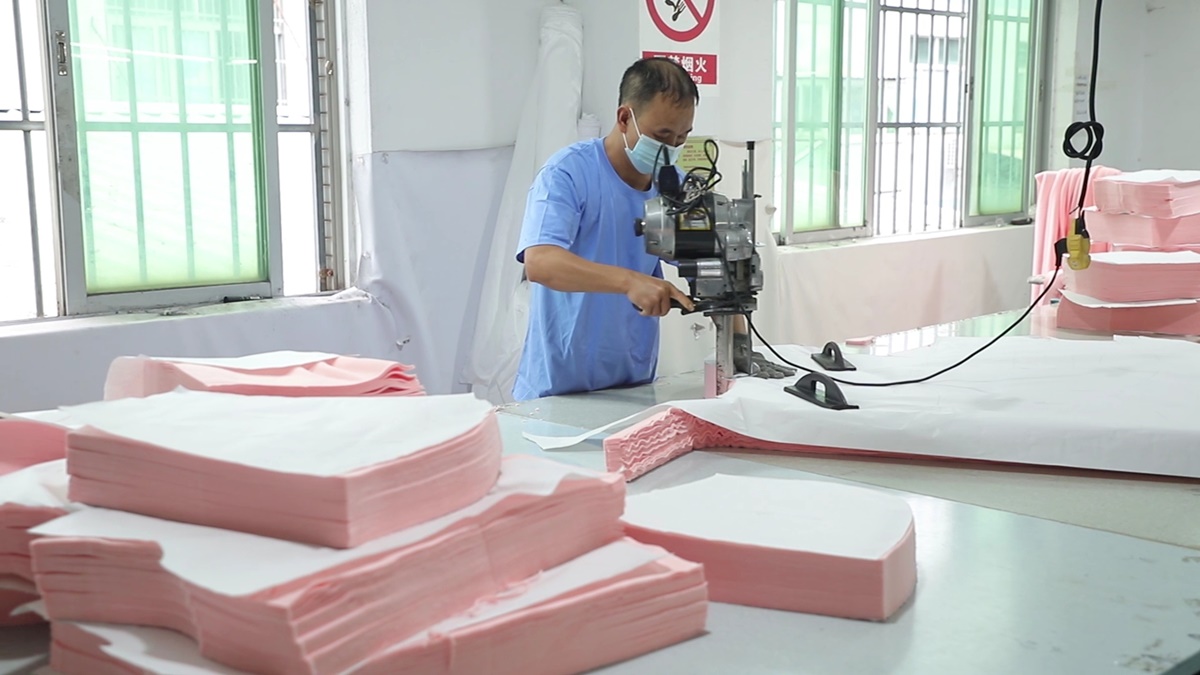
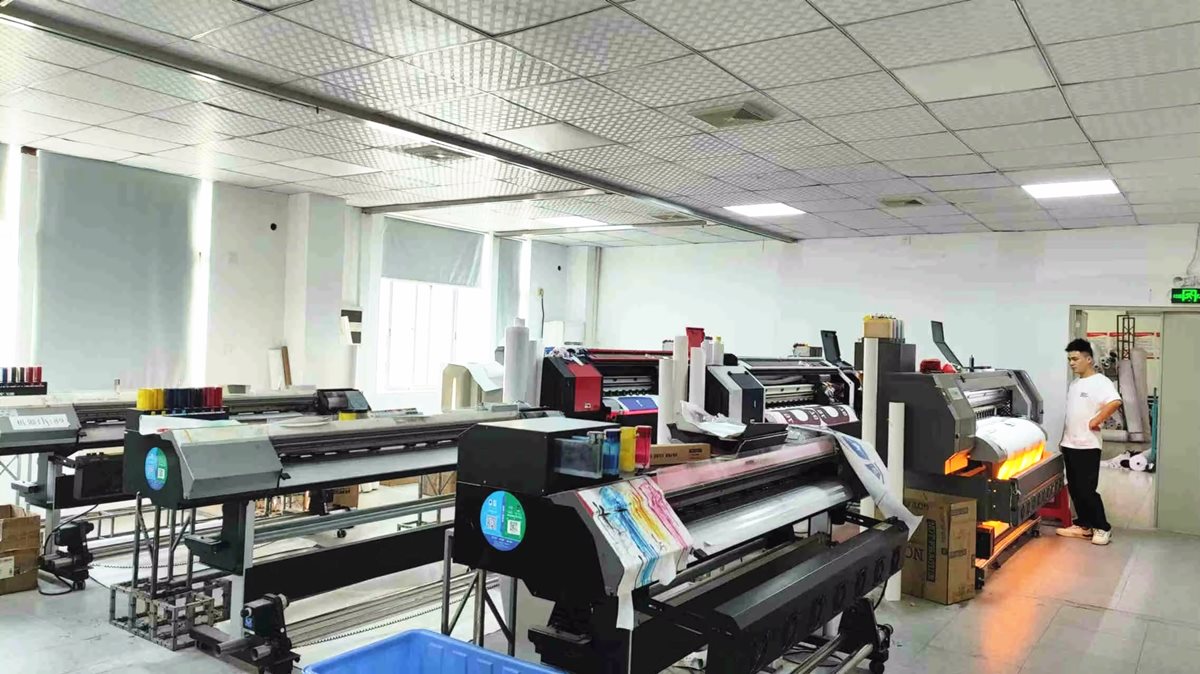
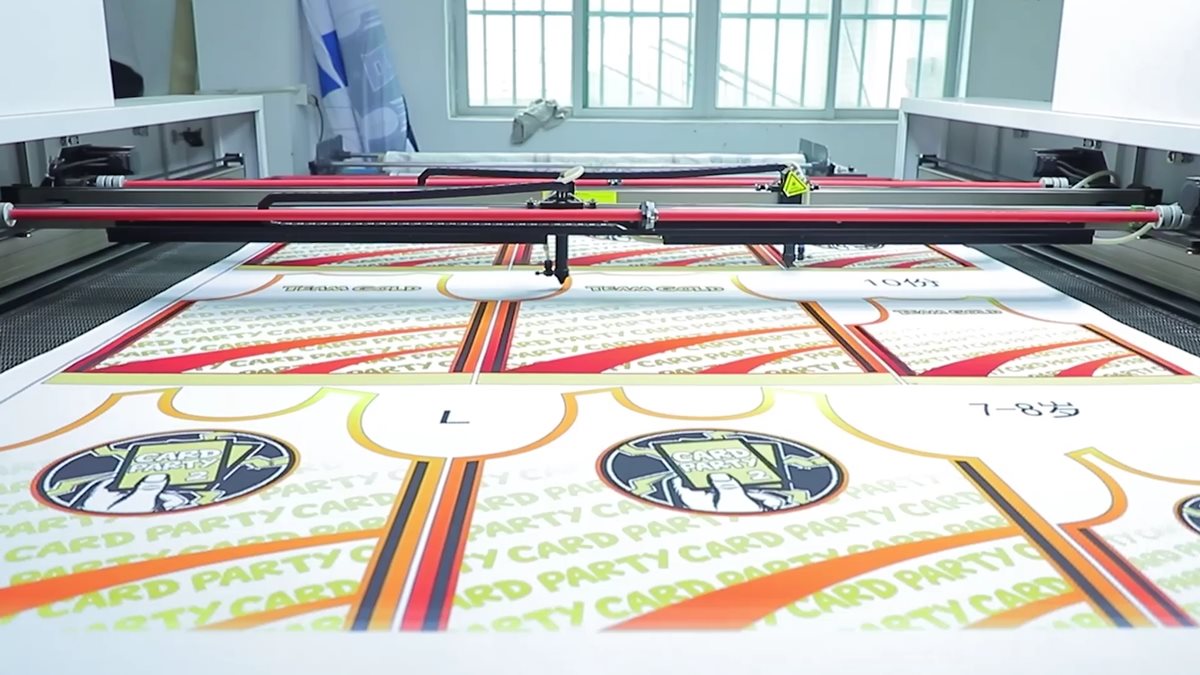
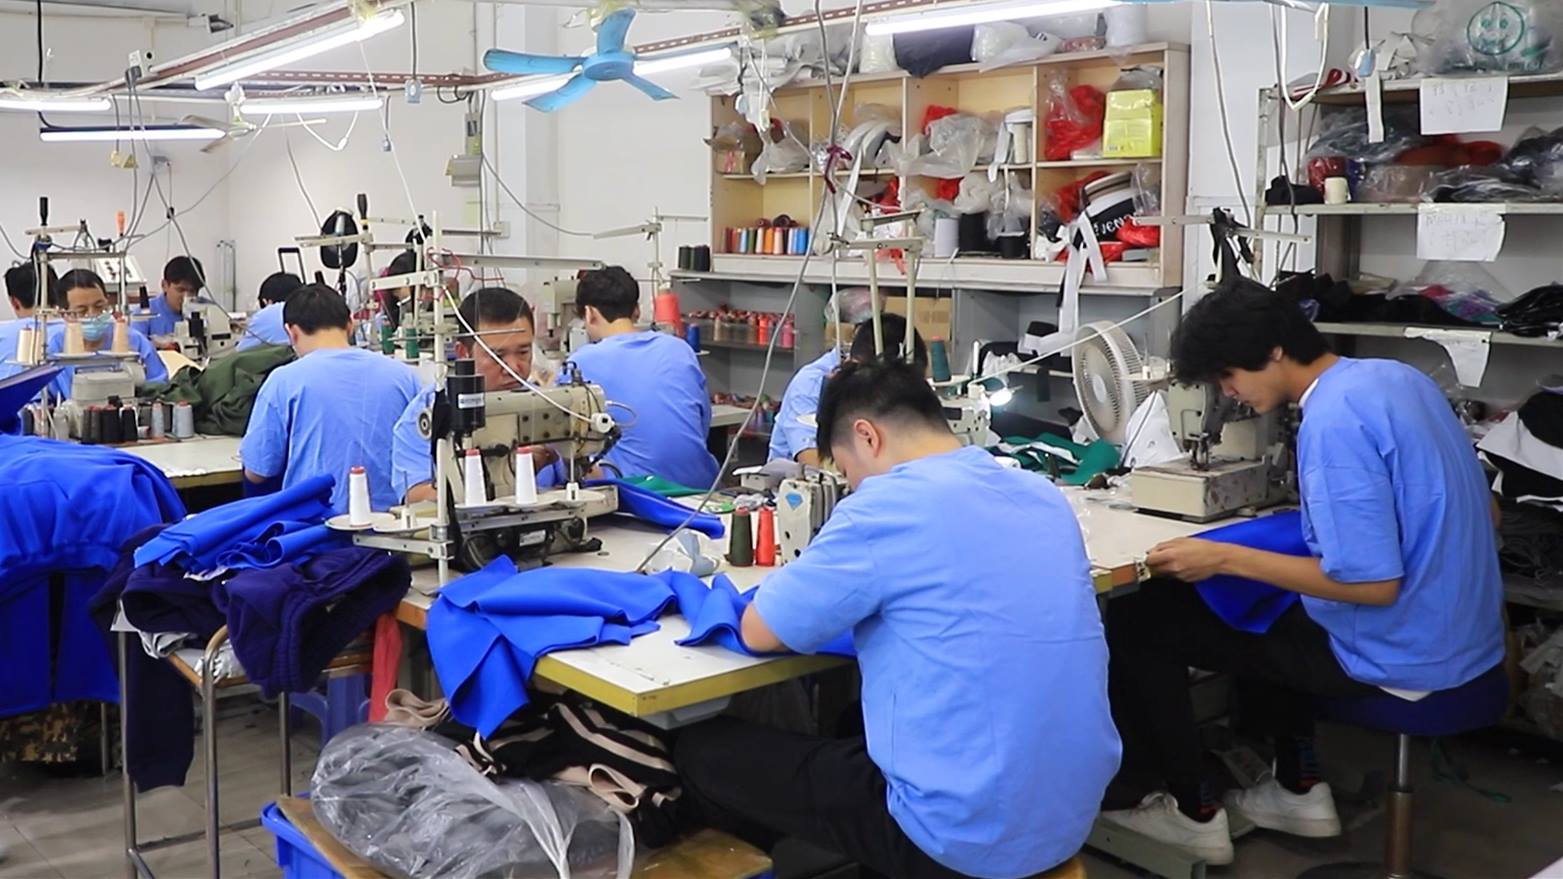
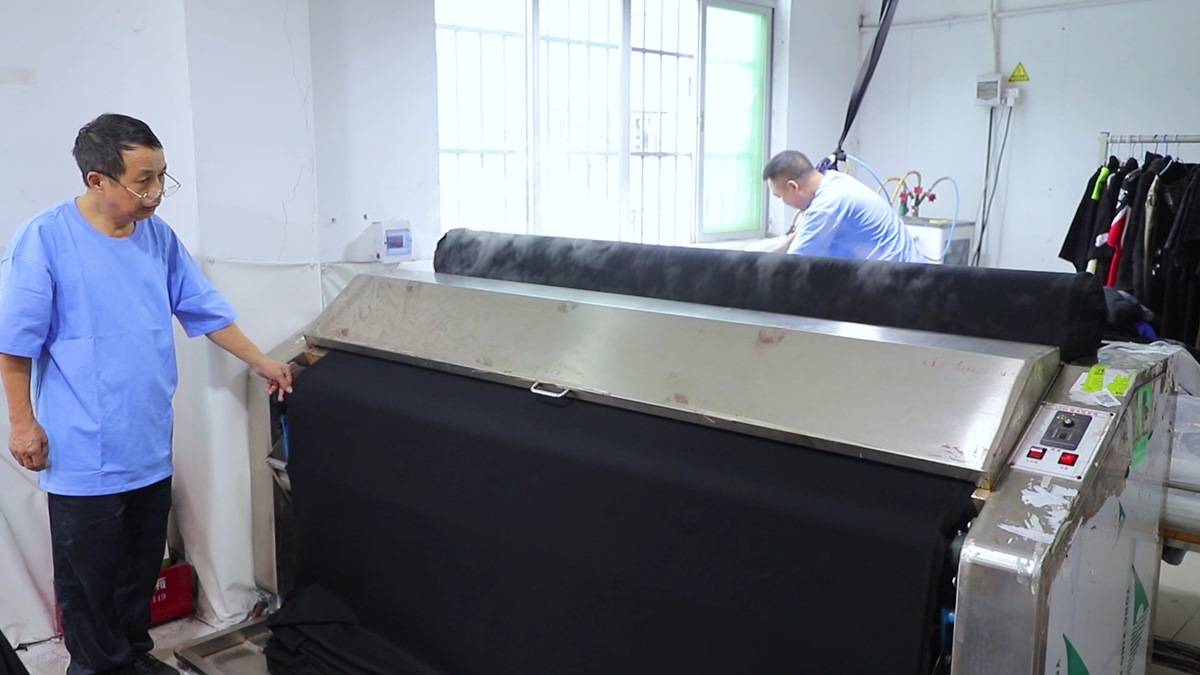
The garment manufacturing paradigm has transitioned from labor-intensive manual operations to high-precision, digitized, and automated processing environments. In our production facilities, we deploy state-of-the-art technological systems to ensure high dimensional accuracy, uniform dye penetration, and structural integrity across large production runs.
This automated digital ecosystem enables low-MOQ capabilities (starting at 2 units for custom styling) and quick-turn sampling without sacrificing precision. By linking advanced ERP planning software to the cutting floor and dye-kitchens, we mitigate textile waste, optimize layout utilization, and accelerate speed-to-market metrics for our global client portfolio.
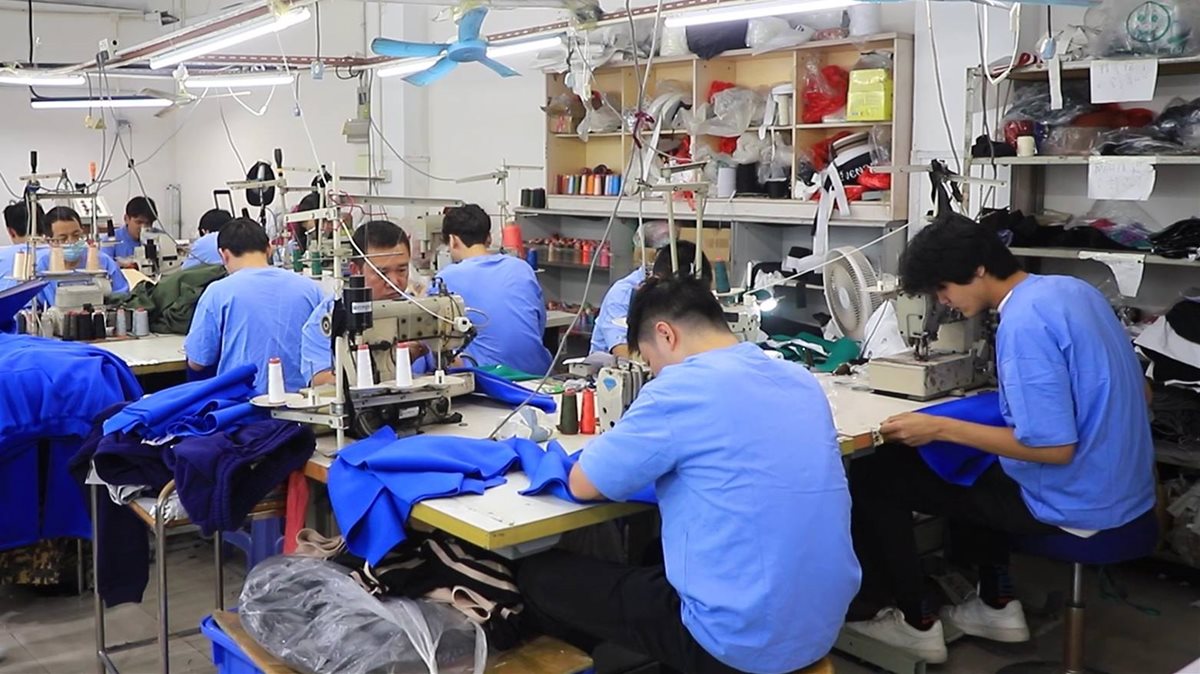
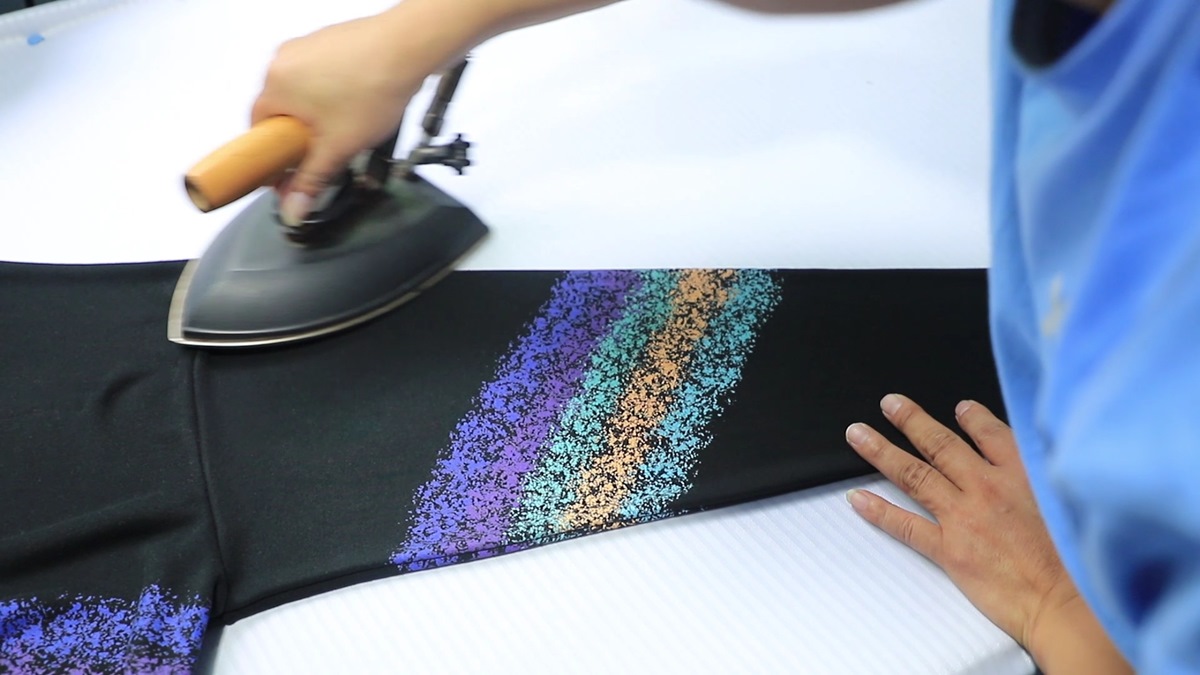
Below is a visual breakdown of our vertically integrated manufacturing facility. Every step—from CAD pattern nested laser cutting to clean-room final packaging—is monitored using IoT sensor arrays and automated quality checkpoints.
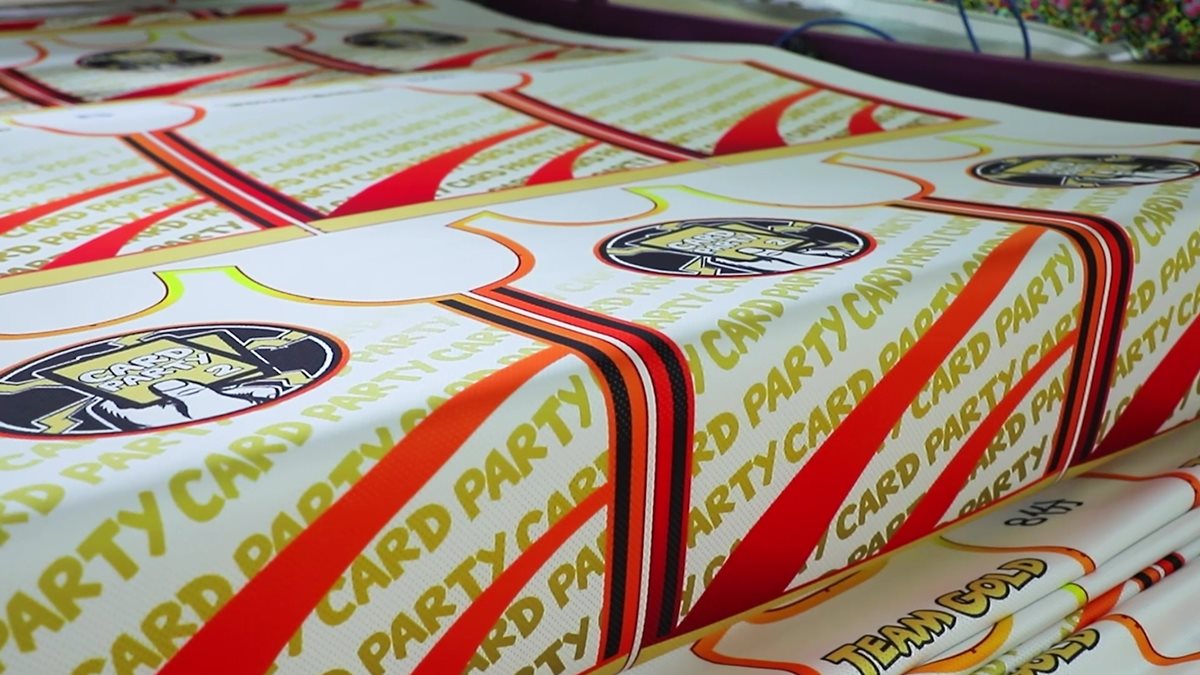
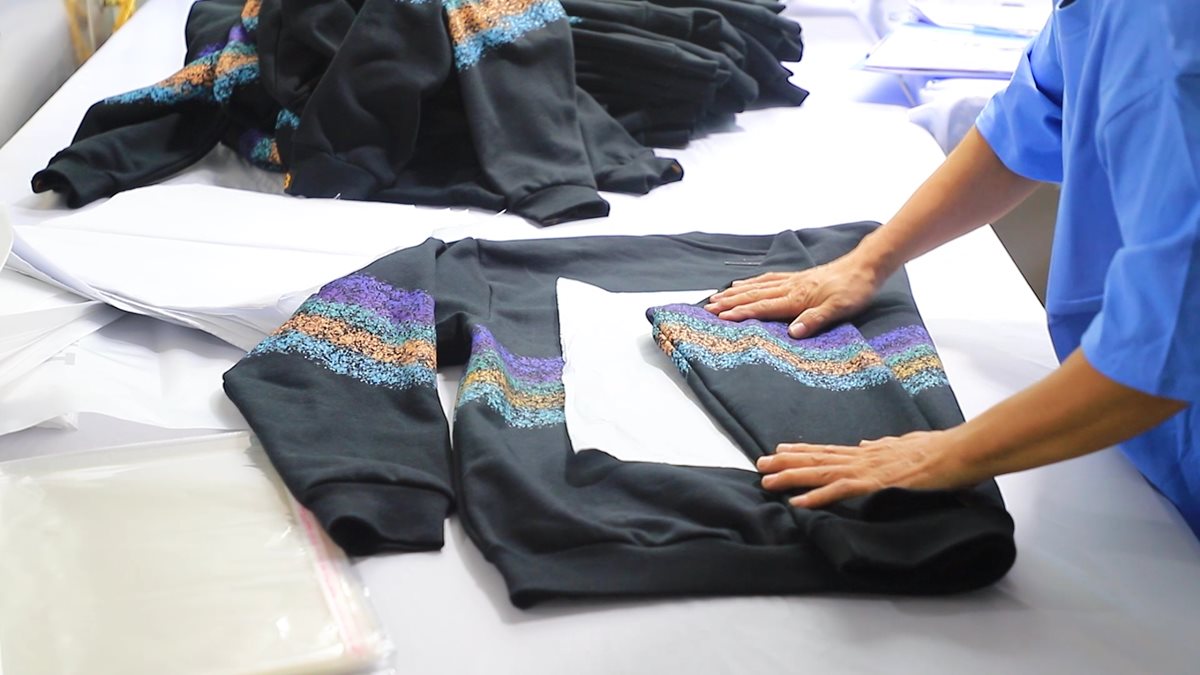
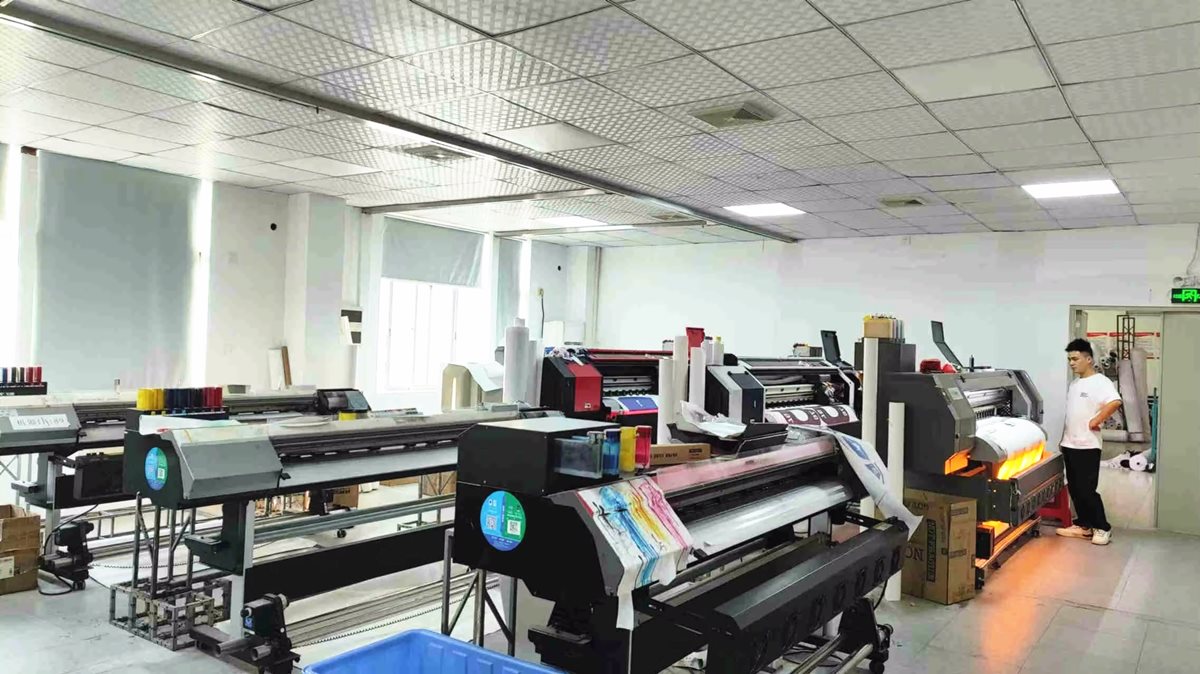
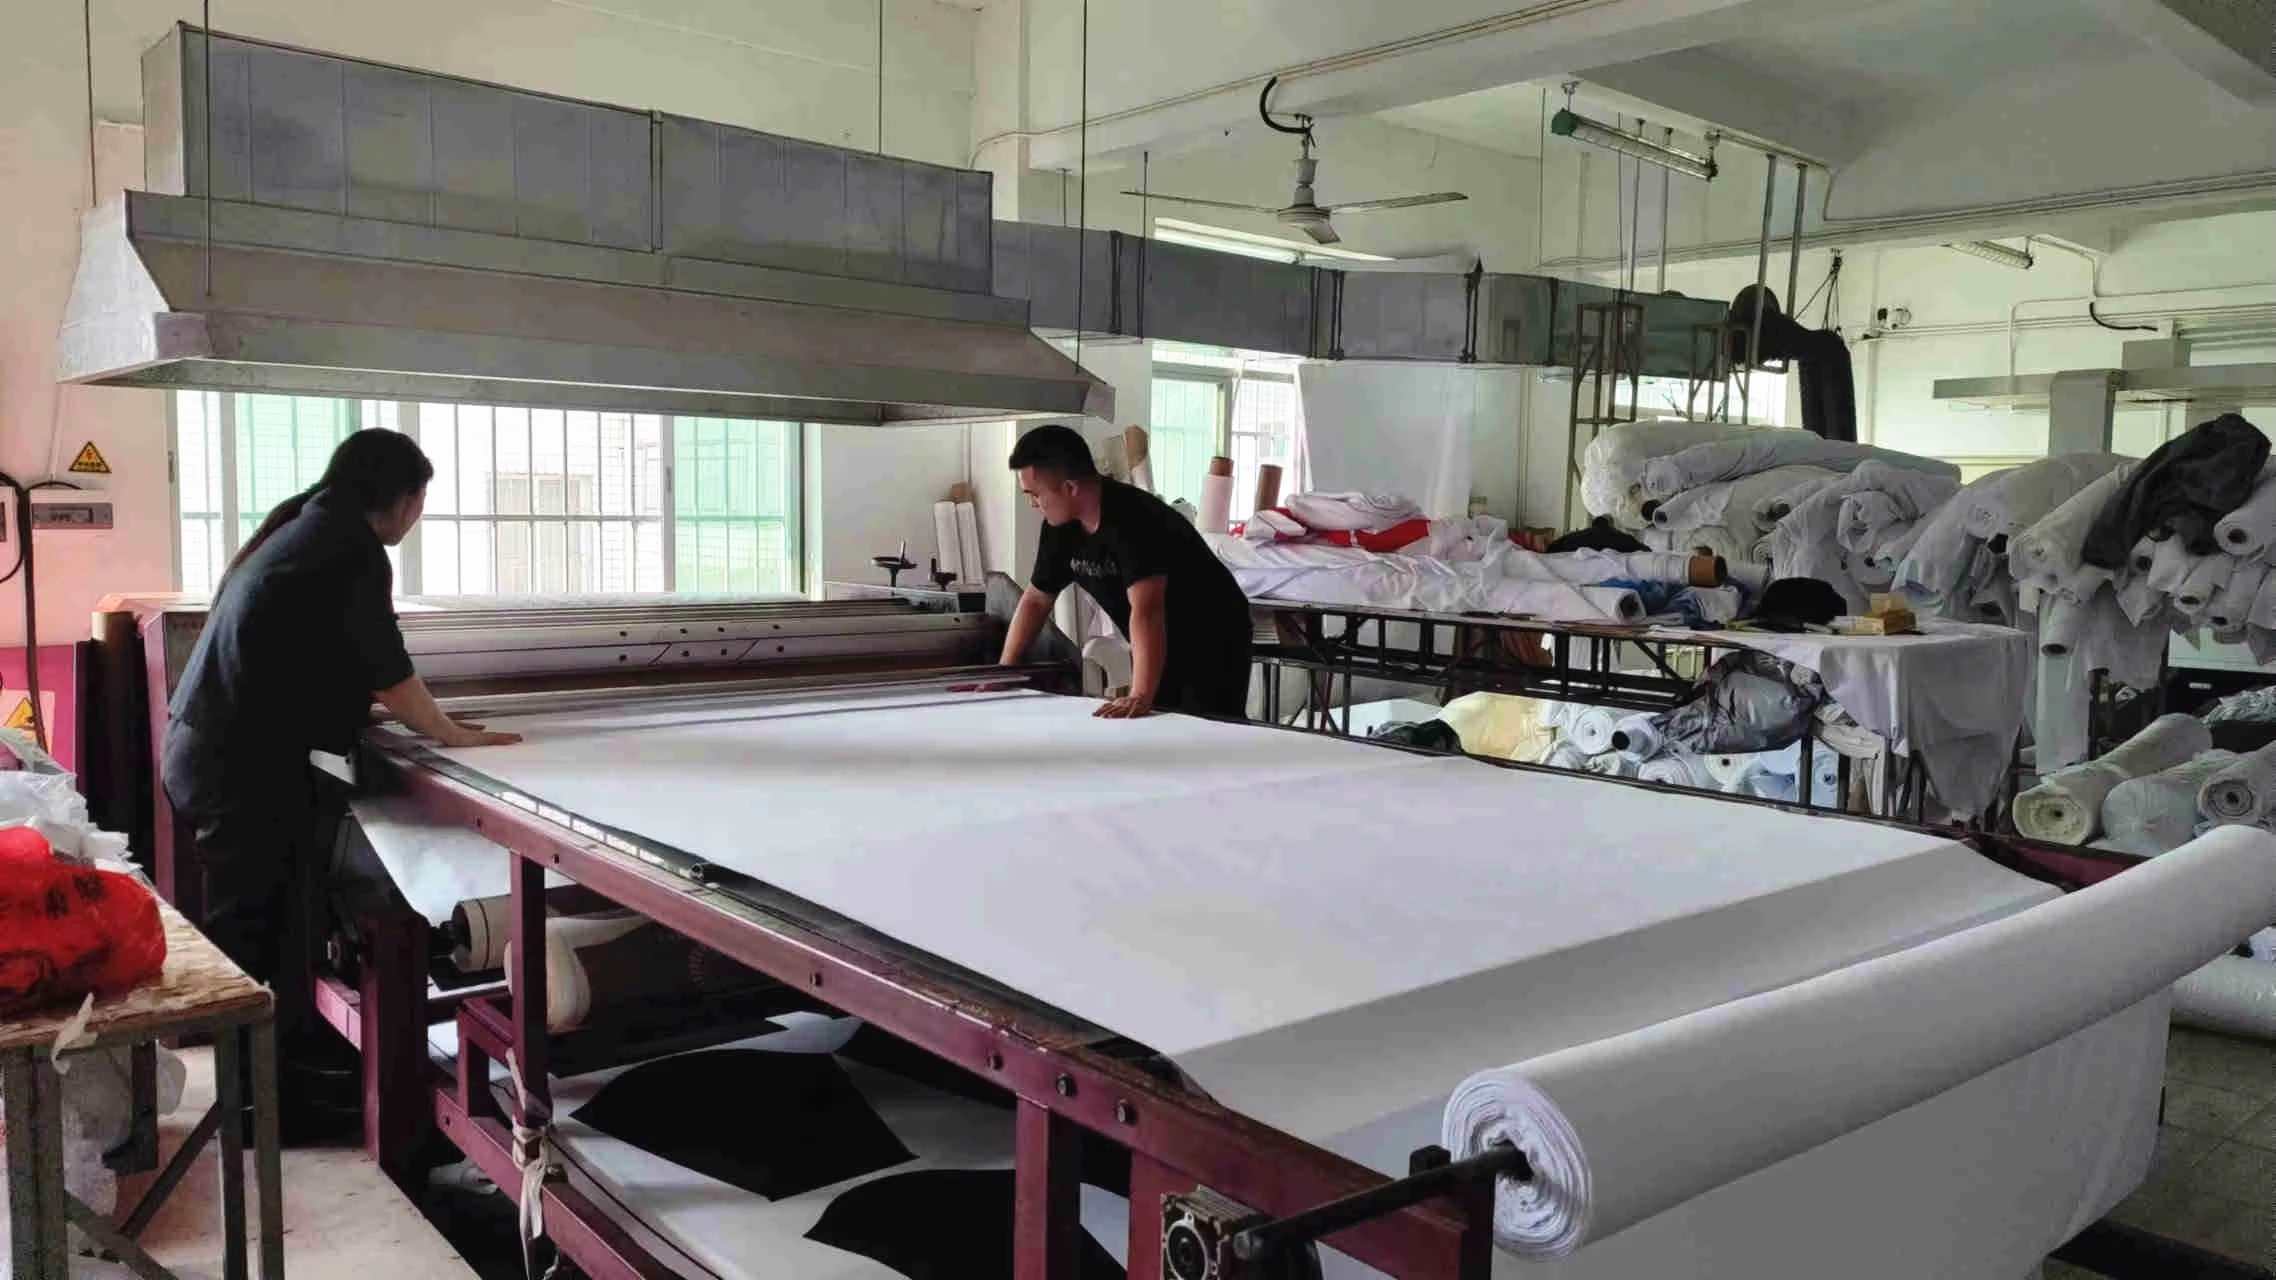
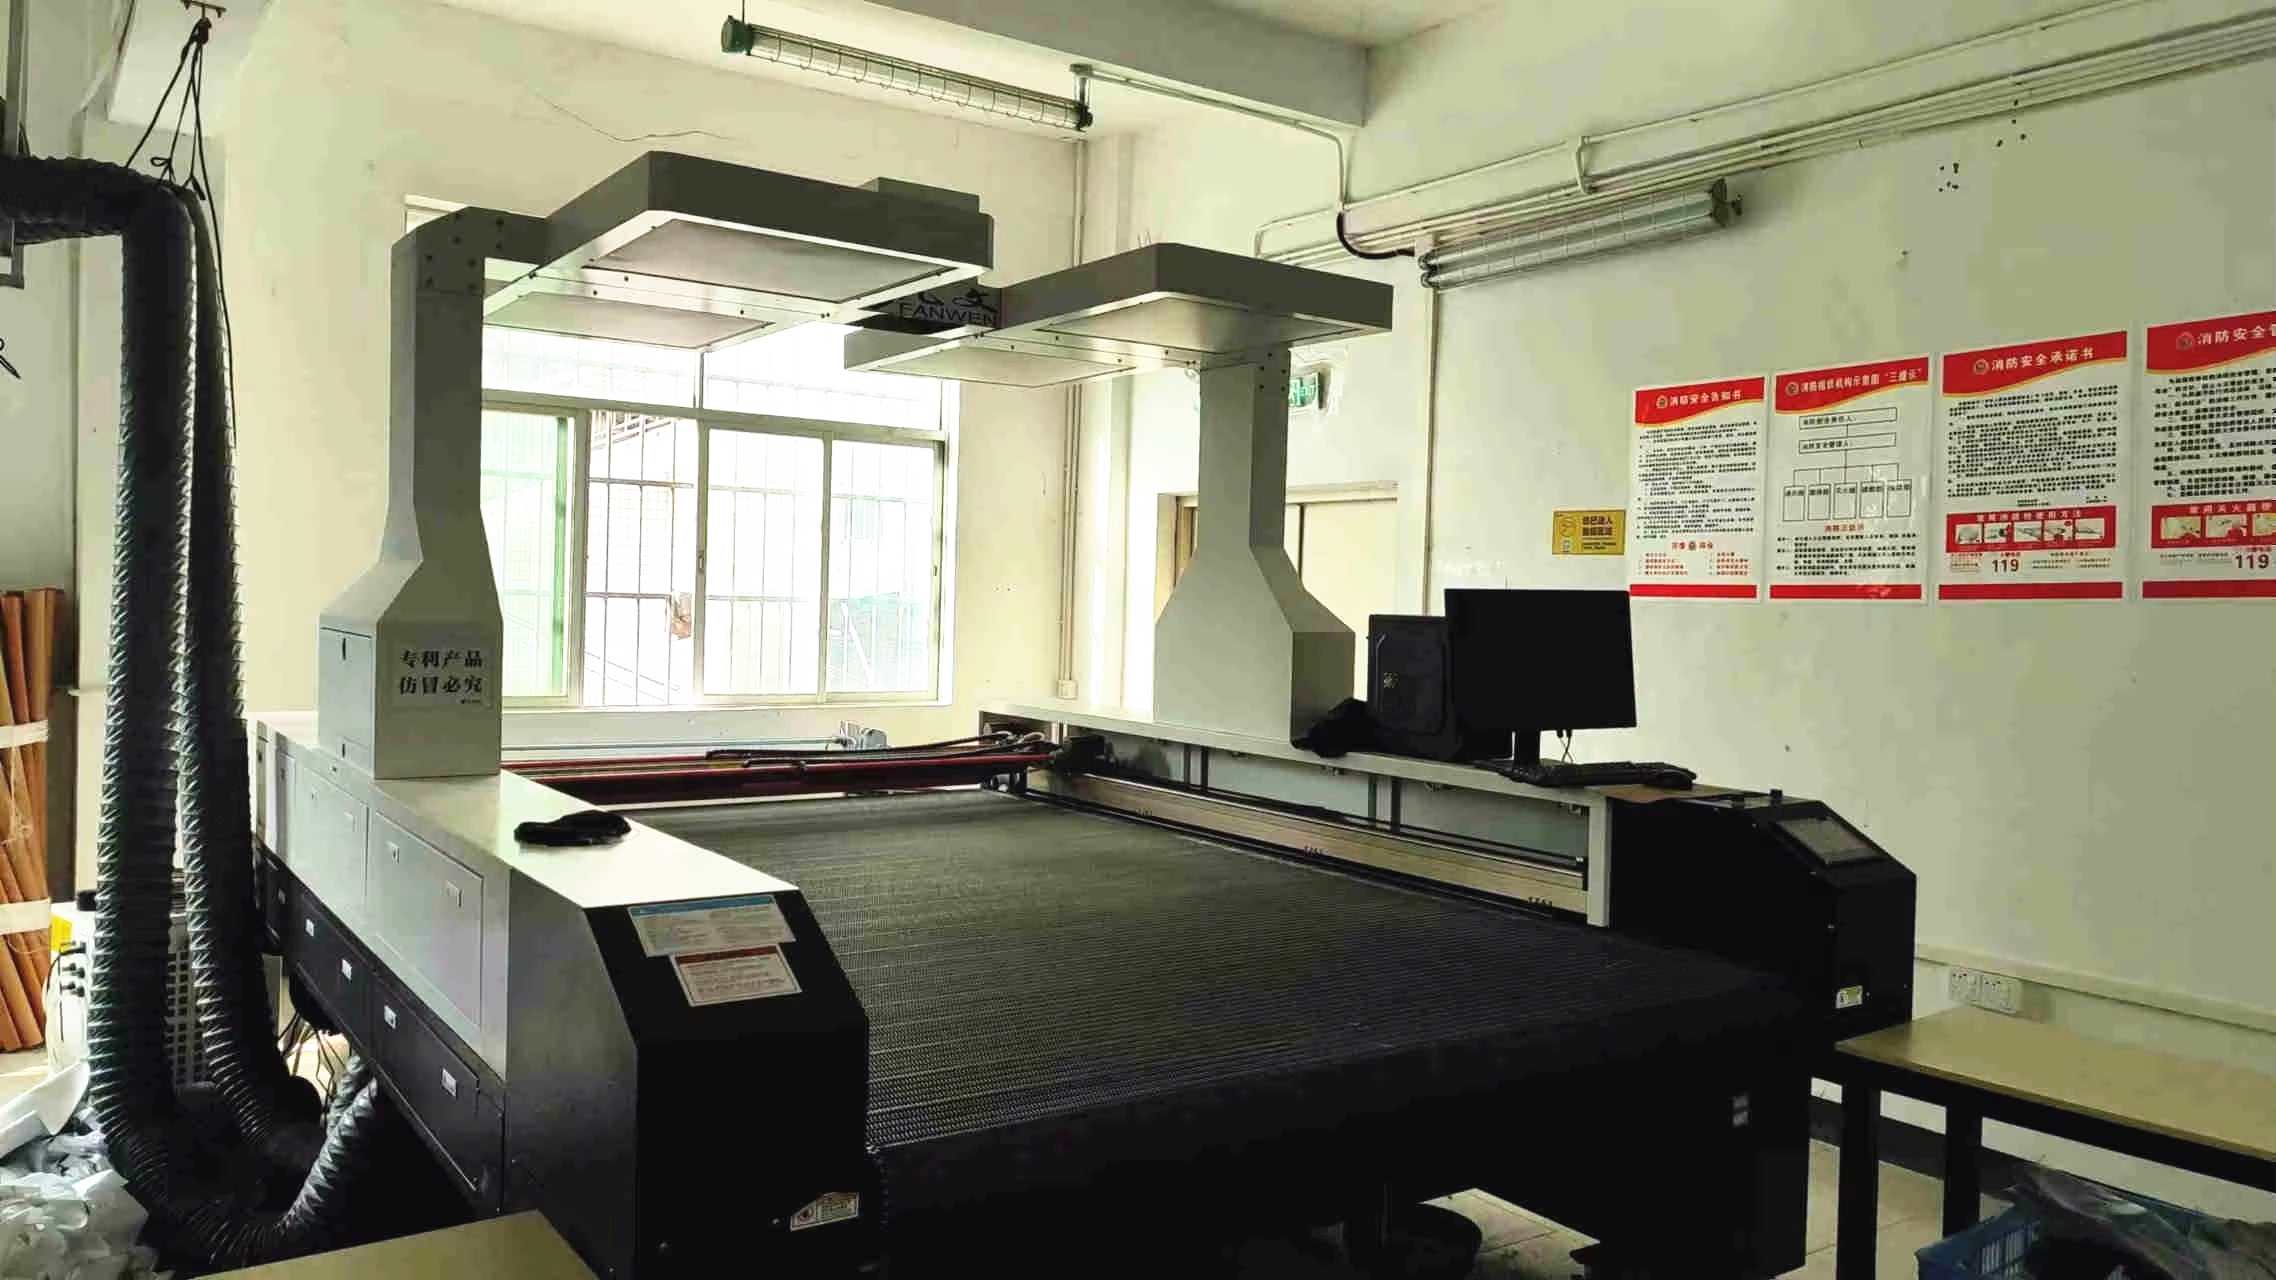
A long sleeve tee's performance depends on the engineering of its yarn. Standard jersey fabrics suffer from torque, where the garment twists around the wearer's torso after a few wash cycles due to residual tension in single-knit structures. We address this by using ring-spun and combed double-jersey or interlock knits, heat-set under controlled tension to ensure balanced recovery characteristics.
Furthermore, cuff execution represents a key failure point in cheap imports. We formulate our wrist ribs using a 95% combed cotton and 5% elastane (Lycra) blend knitted at a higher density (typically 320 GSM). This prevents stretching over extended wear-and-wash cycles.
| Fabric Quality | Composition Breakdown | Optimal Fabric Weight | Primary Commercial Use-Case |
|---|---|---|---|
| Ultra-Soft Premium | 100% Combed Ring-Spun Cotton (Long-Staple) | 160 - 180 GSM | Luxury streetwear layering, high-end private labels. |
| Heavyweight Urban Grit | Open-End / Carded Cotton Blends | 240 - 300 GSM | Oversized boxy fits, structural drops, skater apparel. |
| Performance Eco-Blend | 60% Organic Cotton / 40% Recycled PET Polyester | 180 - 200 GSM | Sustainable corporate uniforms, premium promotional wear. |
| Thermal Waffle Structure | Cotton-Poly Micro-Honeycomb Grid Knit | 220 - 260 GSM | Outdoor thermal layers, tactile lifestyle collections. |
For custom graphic applications, the fabric surface must remain flat and free of loose fibers. We treat our long sleeve knit textiles with bio-polishing enzymes (cellulase enzymes) to eliminate micro-fibrils, preventing pilling. This creates a smooth base for digital direct-to-garment (DTG) printing, high-density plastisol screen printing, or detailed embroidery.
Operating a global brand requires a supply chain partner capable of handling international trade complexities. Sourcing clothing involves navigating international customs codes, regional fiber labeling mandates, and strict import tariffs. We maintain active compliance pipelines to guarantee direct passage through customs in major consumer hubs across North America, the European Union, and the Asia-Pacific region.
Our logistics management teams coordinate with major freight forwarders to provide multimodal transport options, including ocean freight, expedited air options, and door-to-door (DDP) logistics solutions that simplify the import process.
We believe that sustainable manufacturing is essential for long-term growth. Our production facilities maintain standard international certifications, ensuring your brand complies with global environmental and labor laws:
Guangdong NovaFair Fashion Co., Ltd. is a leading professional garment manufacturer in China with over 20 years of experience in the apparel industry. We specialize in the design, development, and production of high-quality and fashion-forward clothing, dedicated to meeting the evolving needs of global markets driven by economic, cultural, and lifestyle changes.
With a strong focus on innovation and flexibility, NovaFair has built a responsive and efficient production system that supports modern business demands, including low MOQ (as low as 2 pieces), fast sample development, competitive pricing, and reliable customer service. These advantages allow us to support designers, brands, and wholesalers with greater agility and creativity.
Over the years, we have cultivated a professional and collaborative team culture rooted in trust, efficiency, and continuous improvement. Our ability to adapt quickly to changing trends and client requirements has enabled us to build long-term partnerships across different regions.
From a small, experience-driven workshop to an internationally oriented apparel manufacturer, NovaFair has continuously evolved with the fashion industry. We embrace change as an opportunity for growth and innovation, constantly improving our craftsmanship, production capability, and service quality.
Today, we proudly serve emerging designers, established brands, and private labels, especially in the North American and European markets, offering customized solutions that bring creative concepts to life.
To become a trusted global partner in fashion manufacturing, empowering designers and brands worldwide with flexible, sustainable, and high-quality apparel solutions—especially in the field of customized denim and contemporary fashion wear.
We are guided by the values of customer-first, integrity, unity, adaptability, passion, professionalism, and shared growth.
Our mission is to deliver exceptional garments and reliable manufacturing solutions while building long-term partnerships based on trust, creativity, and mutual success.
Technical responses regarding manufacturing capabilities, logistics lead times, and global shipping policies.
High-demand activewear, vintage thermal knits, and functional street fashion manufactured to rigorous international standards.
 NovaFair Fashion