Explore our curated export-grade garments featuring high-density knits, moisture-wicking synthetic blends, and precision-engineered casual athleisure styles developed for global distributors and private labels.


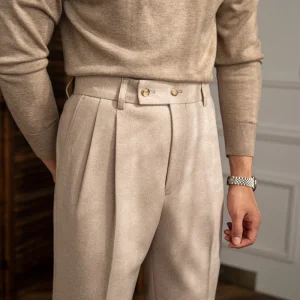


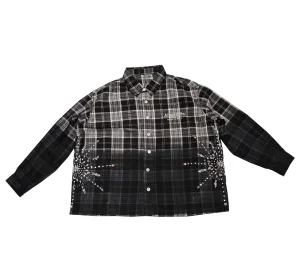
The global athleisure wear market has crossed a monumental watershed, expanding beyond a niche lifestyle trend into a dominant $350+ billion apparel vertical. Modern consumers demand garments that seamlessly bridge high-intensity workout performance with sophisticated daily streetwear aesthetics. This shift requires apparel manufacturers to possess dual technical masteries: high-precision synthetic fabric engineering (4-way stretch, thermal regulation, moisture management) and high-fashion garment construction (tailored silhouettes, bonded seams, custom dye wash treatments).
Eliminating bulky stitched seams using ultrasonic welding and thermo-bonded tape reduces skin friction during movement while delivering ultra-clean, minimalist aesthetics demanded by luxury streetwear brands.
Procurement focus has shifted toward GRS-certified recycled nylon 6,6, rPET (recycled polyester from ocean plastic), and biodegradable elastane blends that maintain elasticity without shedding microplastics.
Leading D2C brands are abandoning traditional 5,000-piece MOQs. Manufacturing partners offering agile batch sizes (down to 2–50 pieces) significantly mitigate inventory risk and shorten speed-to-market cycles.
While apparel manufacturing has partially decentralized across Southeast Asia, China retains an unassailable technological and operational advantage in high-performance athleisure wear. The synthesis of complete upstream-to-downstream supply chains, rapid prototyping infrastructure, and state-of-the-art machinery makes China the primary strategic nexus for global activewear brands.
Information Gain Insight: The true bottleneck in functional garment production is not sewing labor cost; it is functional fabric R&D, chemical finishing consistency, and trim lead time. China controls over 70% of global synthetic yarn texturizing and specialized finishing mill capacity (anti-odor silver ion, water-repellent DWR, and phase-change thermal regulation).
In provinces like Guangdong and Zhejiang, functional fabric knitting mills, specialized dye houses, laser-cutting labs, and custom zipper/elastic hardware manufacturers operate within a 50-kilometer radius, slashing sampling times from months to days.
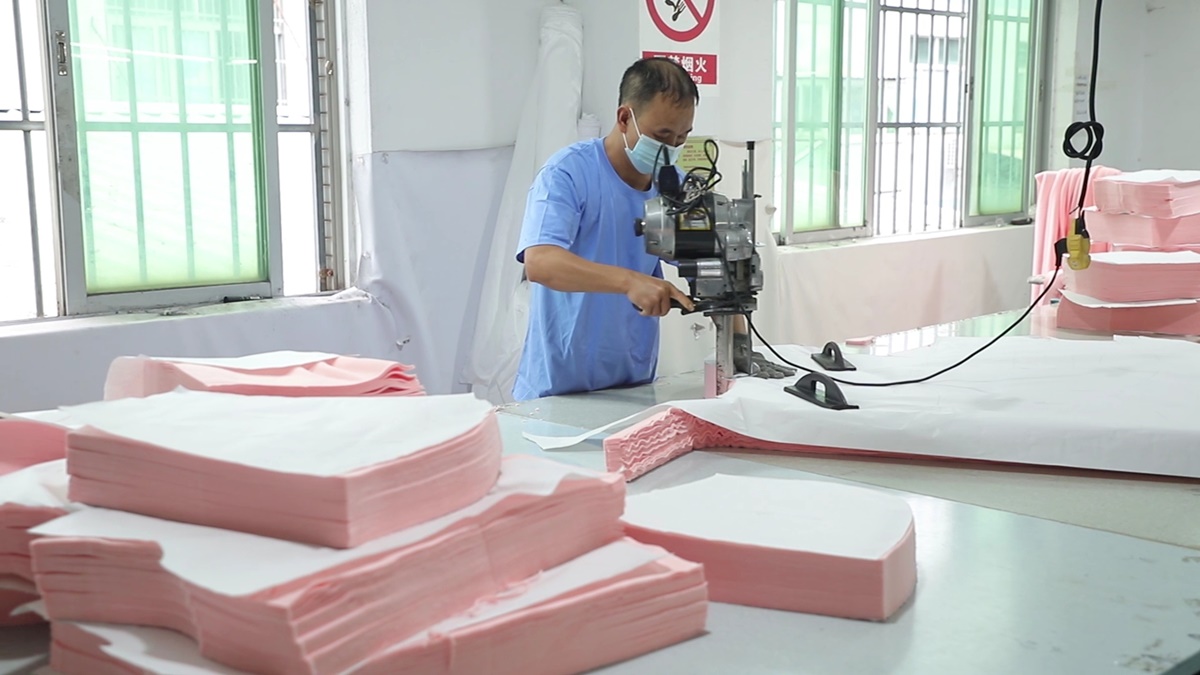
Chinese factories lead in the deployment of automated computer-controlled cutting (CAM) beds, 4-needle 6-thread flatlock stitching systems, and robotic heat-transfer logo applicators, resulting in defect rates below 0.5% (AQL 1.5 standard).
By utilizing 3D digital fitting tools (CLO3D, Optitex), Chinese OEM factories convert digital CAD designs into virtual samples within 48 hours, enabling global procurement teams to finalize tech packs without waiting for physical international freight cycles.
Guangdong NovaFair Fashion Co., Ltd. is a leading professional garment manufacturer in China with over 20 years of experience in the apparel industry. We specialize in the design, development, and production of high-quality and fashion-forward clothing, dedicated to meeting the evolving needs of global markets driven by economic, cultural, and lifestyle changes.
With a strong focus on innovation and flexibility, NovaFair has built a responsive and efficient production system that supports modern business demands, including low MOQ (as low as 2 pieces), fast sample development, competitive pricing, and reliable customer service. These advantages allow us to support designers, brands, and wholesalers with greater agility and creativity.
Over the years, we have cultivated a professional and collaborative team culture rooted in trust, efficiency, and continuous improvement. Our ability to adapt quickly to changing trends and client requirements has enabled us to build long-term partnerships across different regions.
From a small, experience-driven workshop to an internationally oriented apparel manufacturer, NovaFair has continuously evolved with the fashion industry. We embrace change as an opportunity for growth and innovation, constantly improving our craftsmanship, production capability, and service quality. Today, we proudly serve emerging designers, established brands, and private labels, especially in the North American and European markets, offering customized solutions that bring creative concepts to life.
To become a trusted global partner in fashion manufacturing, empowering designers and brands worldwide with flexible, sustainable, and high-quality apparel solutions—especially in the field of customized denim and contemporary fashion wear, extending seamlessly into technical performance athleisure.
We are guided by the values of customer-first, integrity, unity, adaptability, passion, professionalism, and shared growth.
Our mission is to deliver exceptional garments and reliable manufacturing solutions while building long-term partnerships based on trust, creativity, and mutual success.
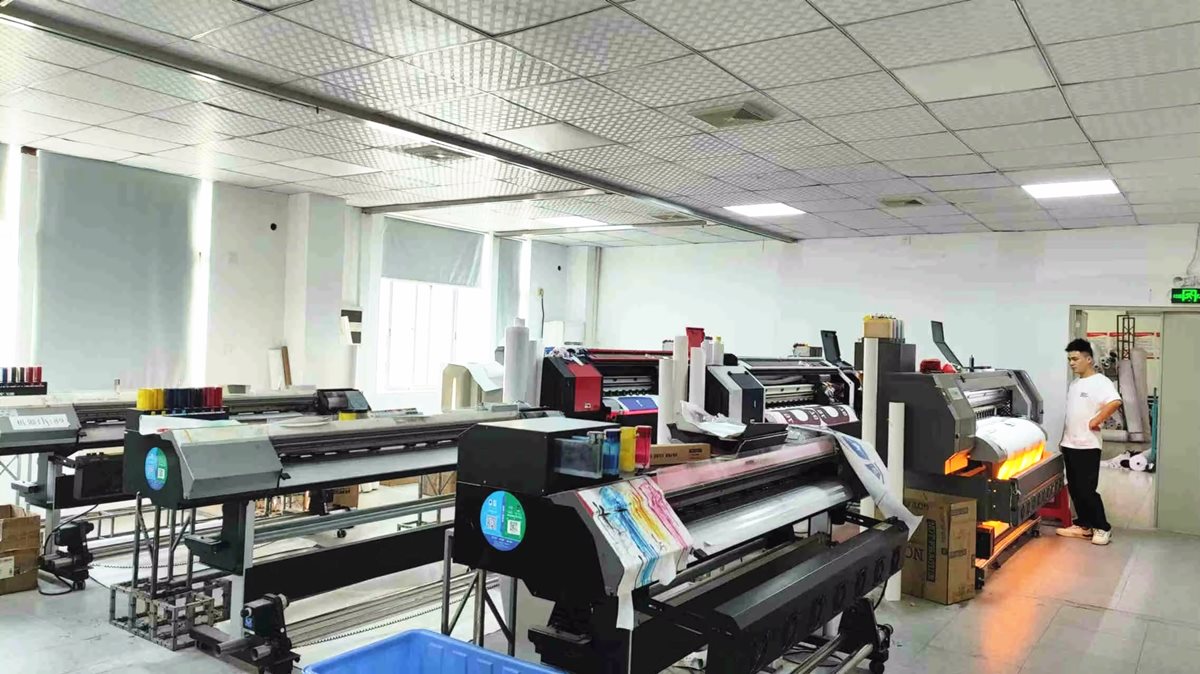
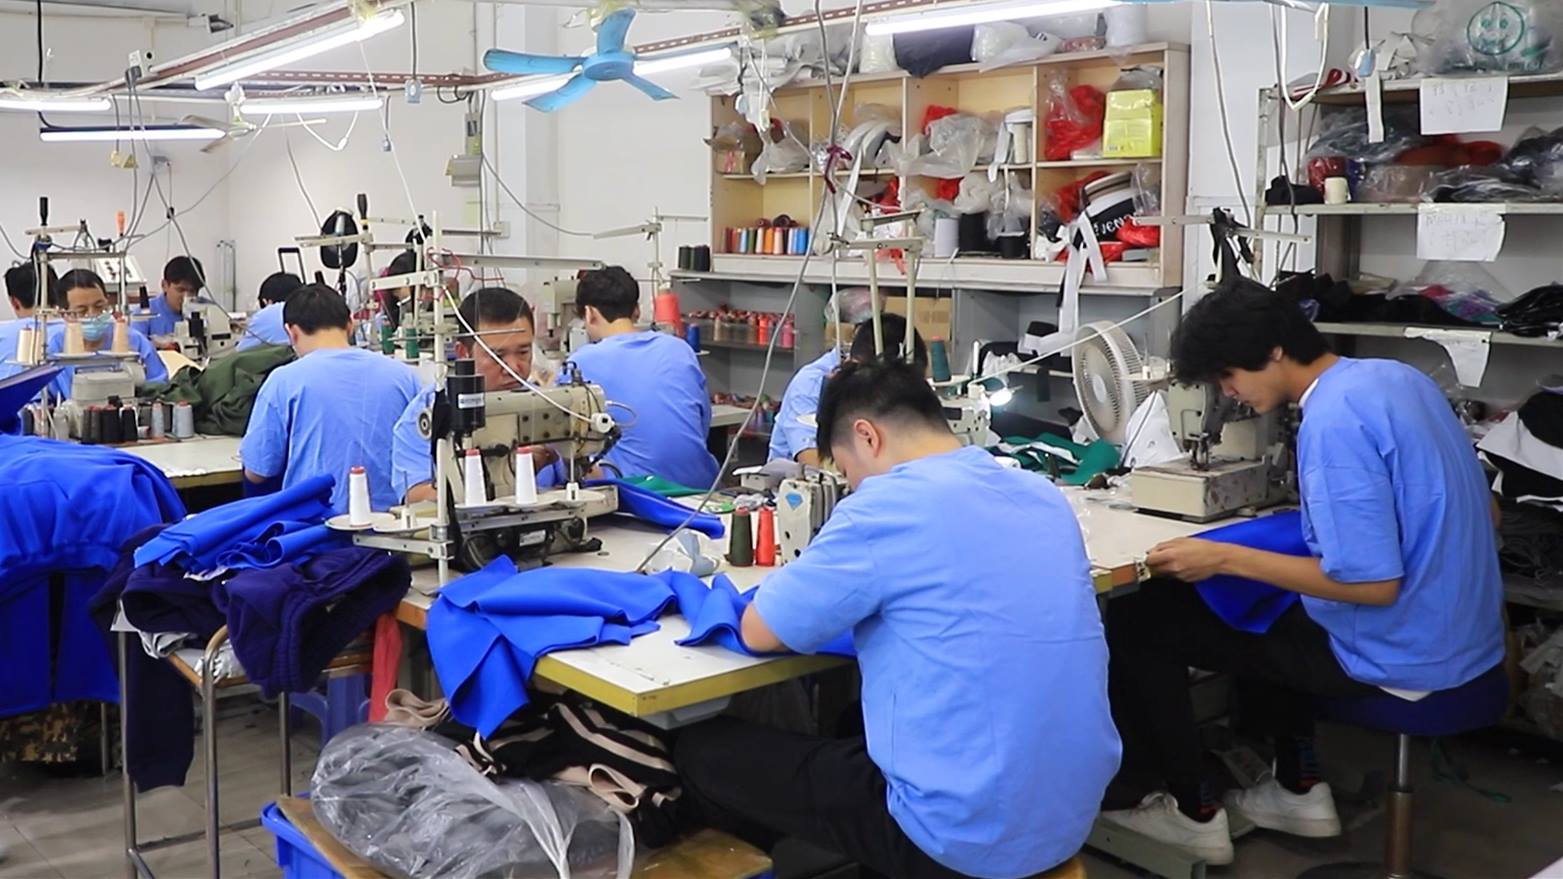
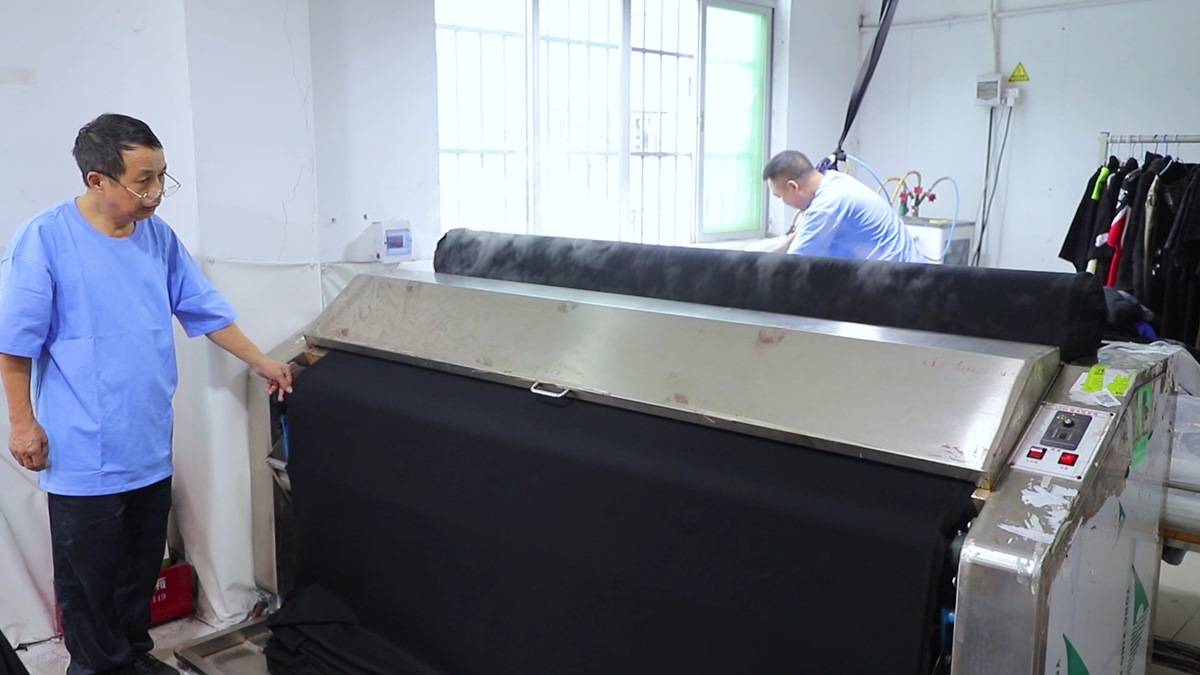
Our state-of-the-art facility in Guangdong features fully automated precision hardware to guarantee strict dimensional stability, flawless seam construction, and fast turnaround across all apparel lines:
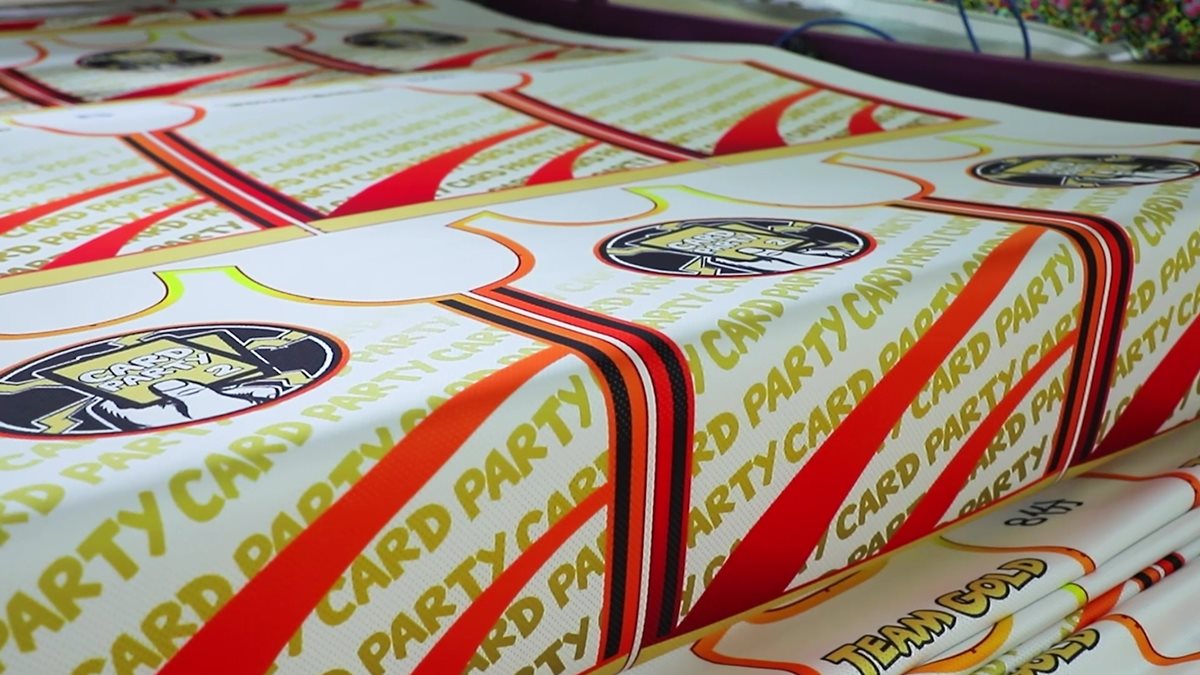
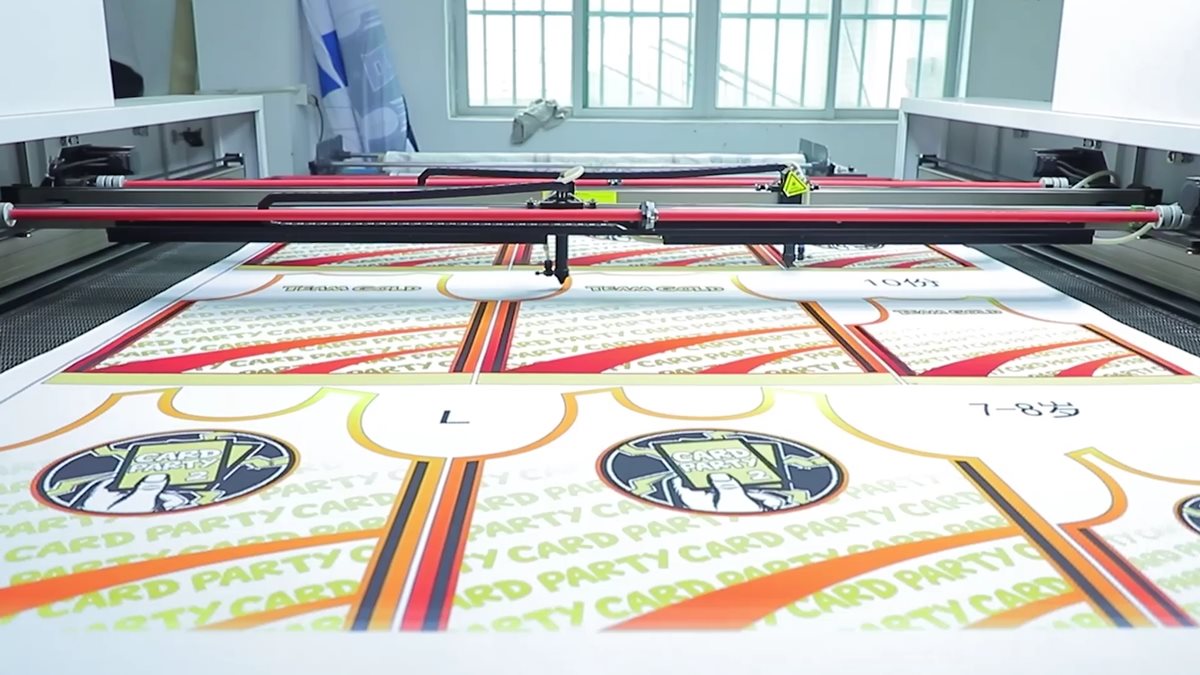
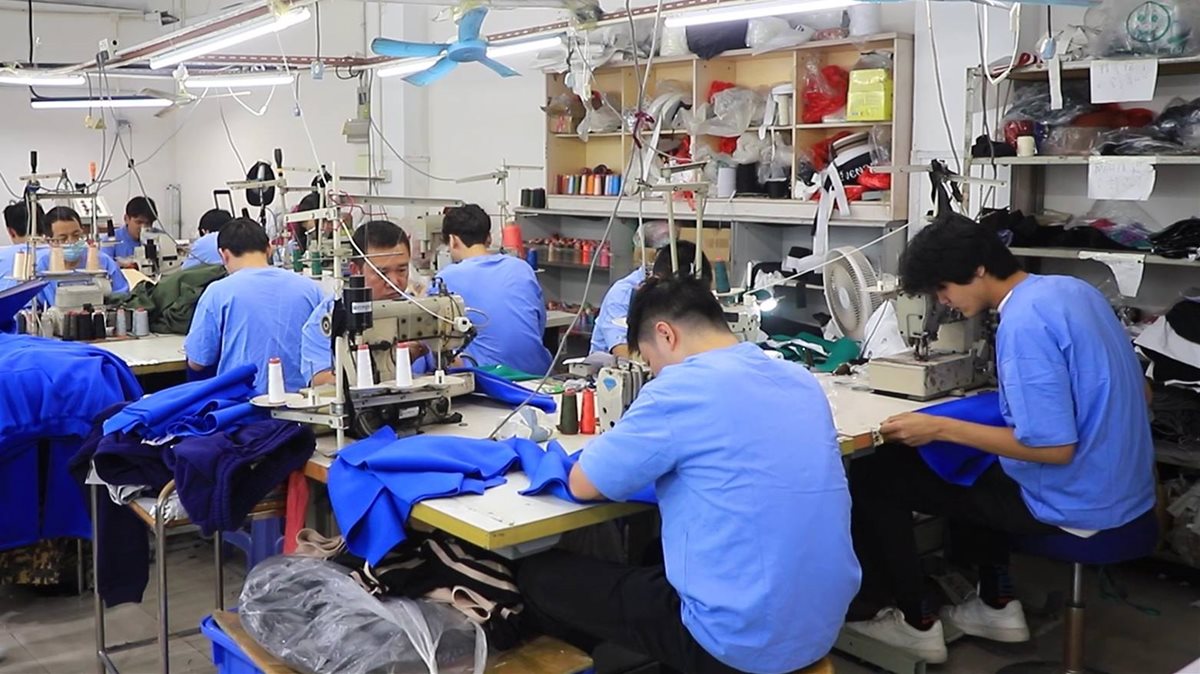
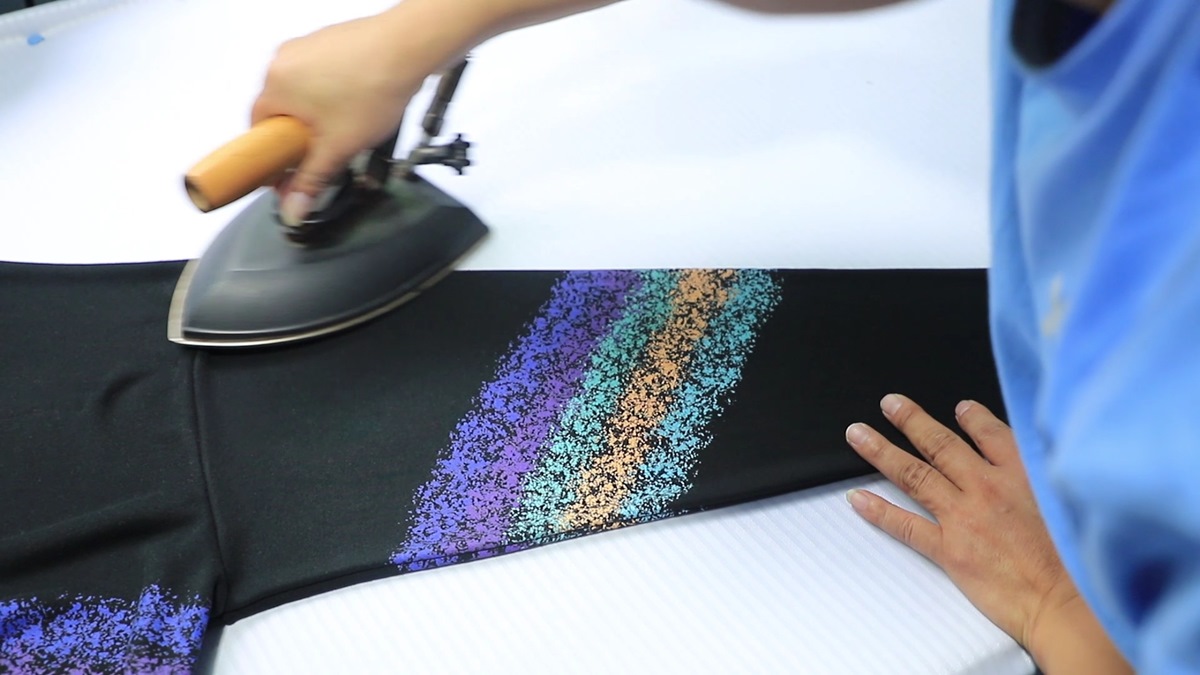
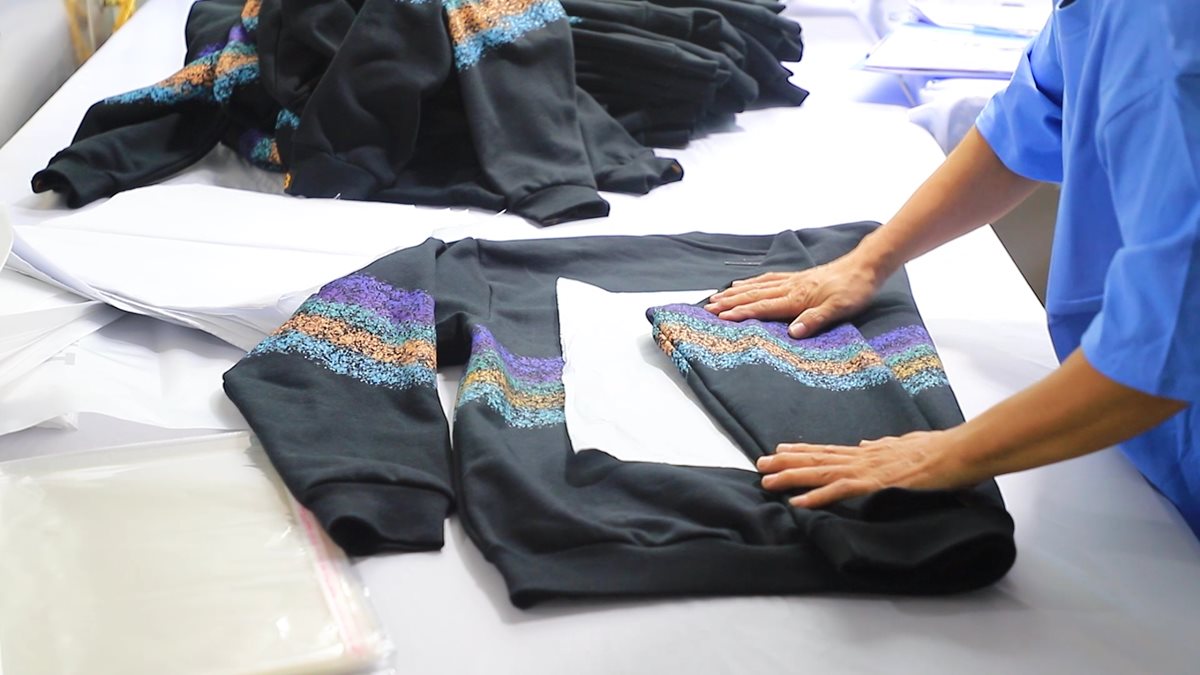
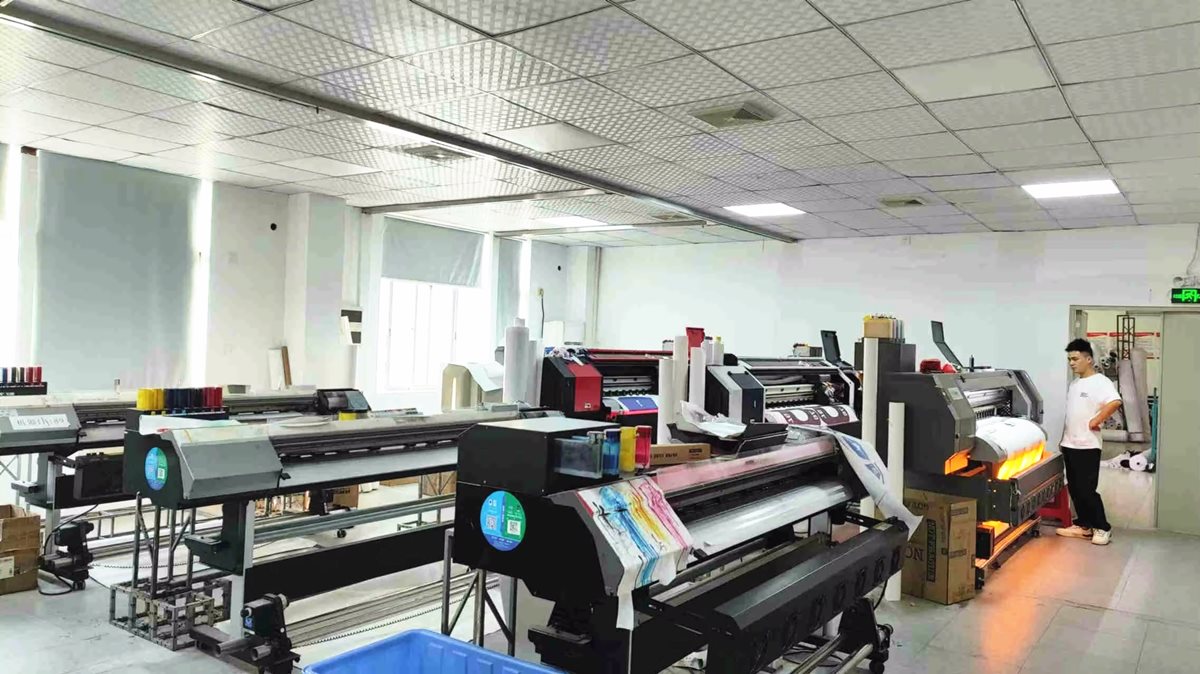
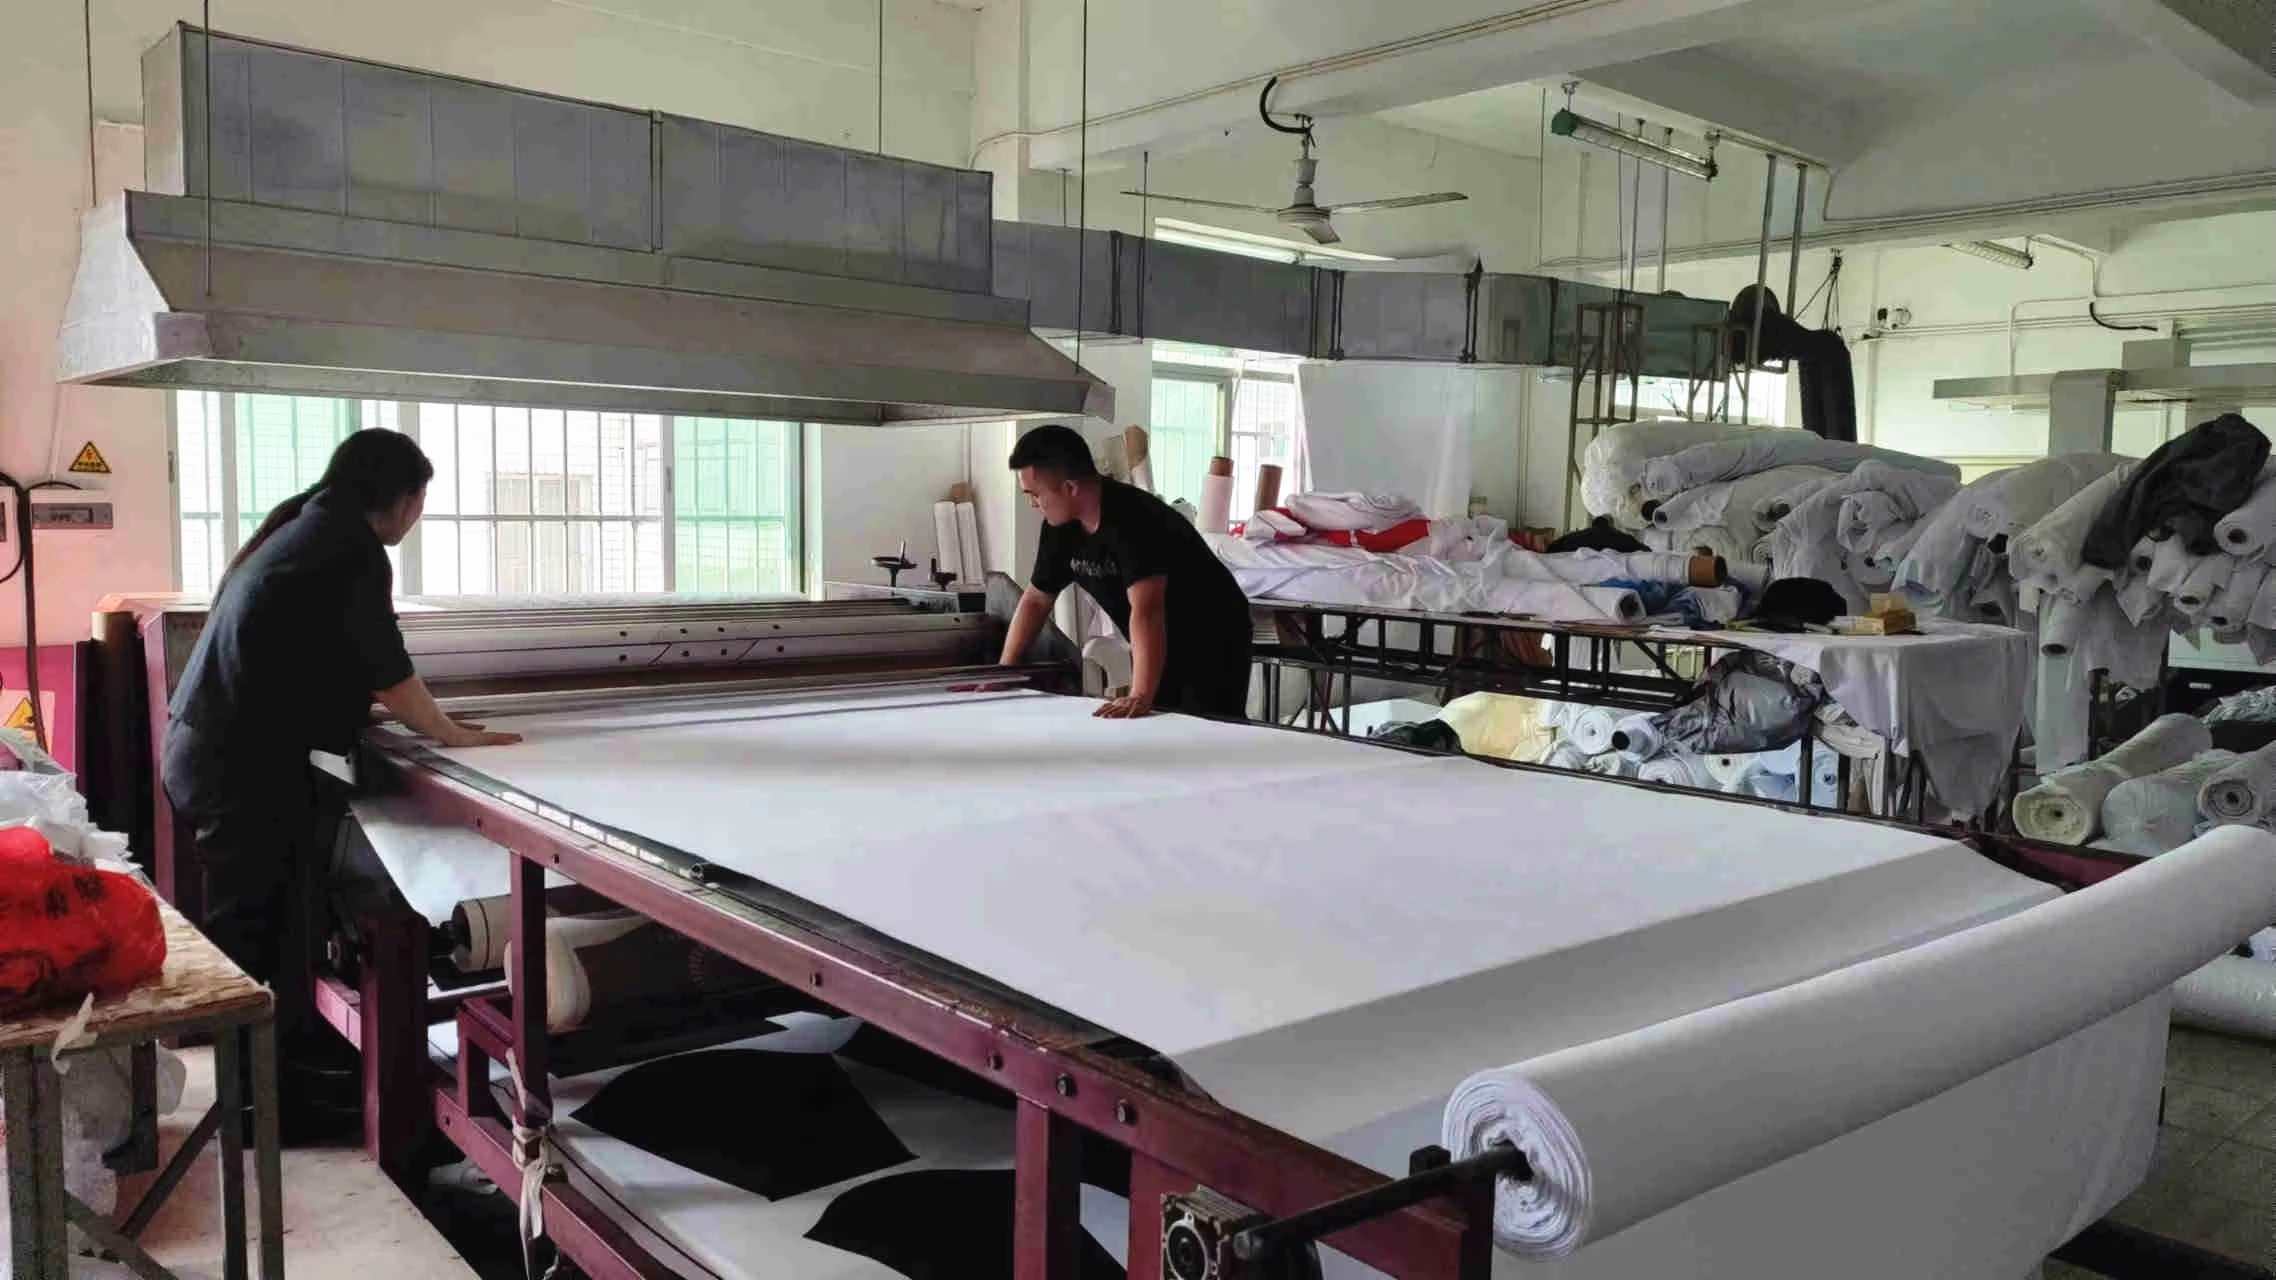
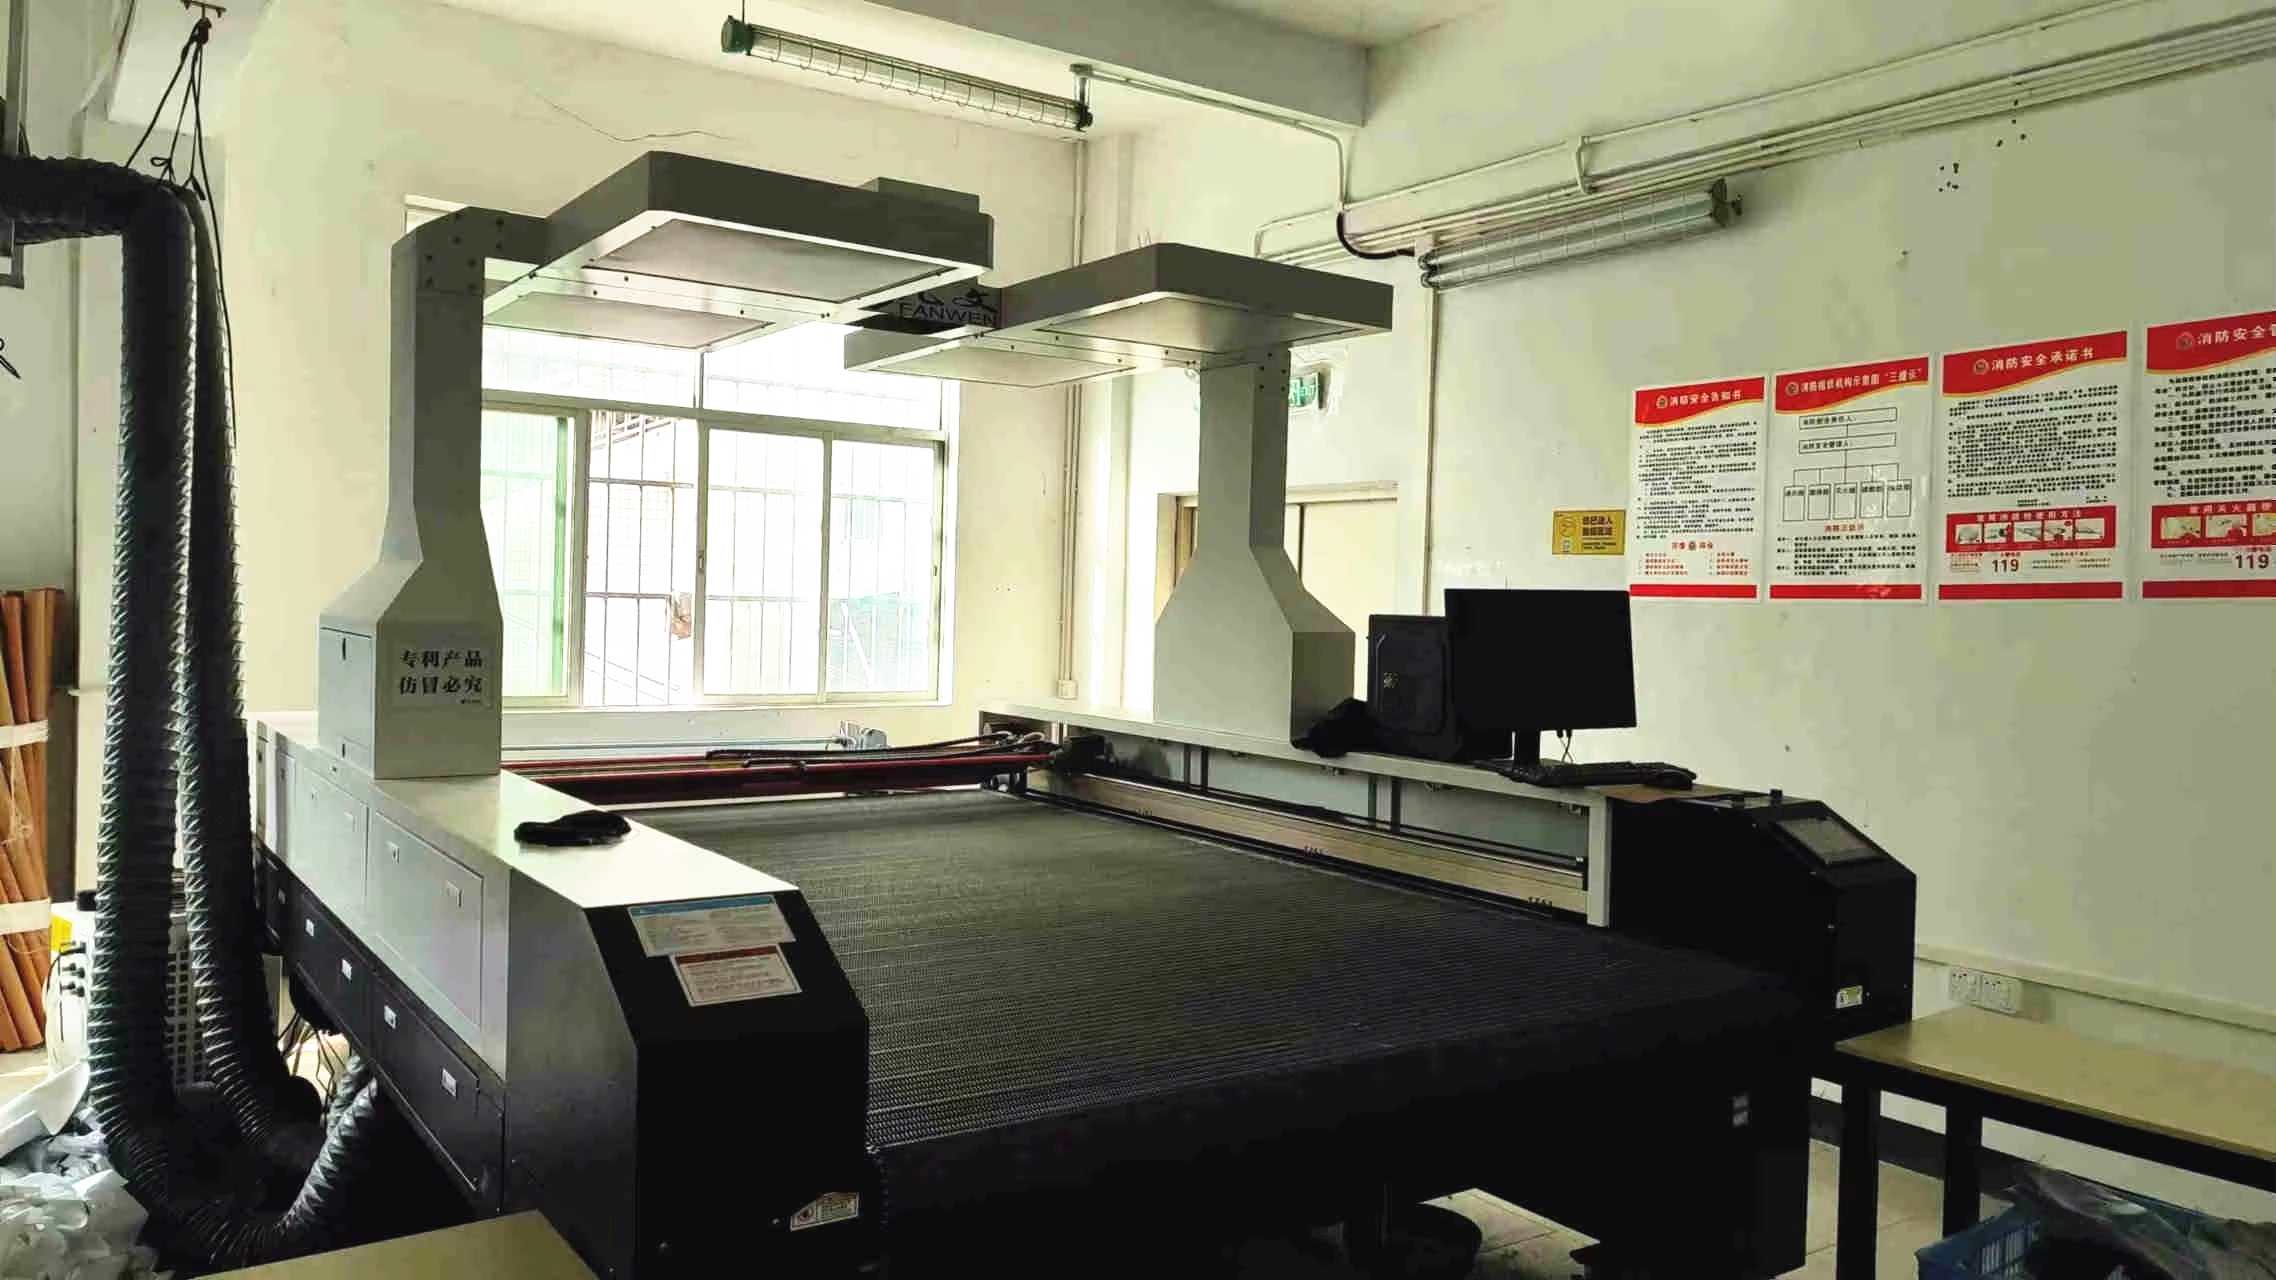
Based on expert audit metrics—including operational capacity, technical compliance, speed of prototyping, minimum order flexibility, and fabric R&D leadership—we have compiled and benchmarked the industry’s top 10 apparel manufacturers and exporters globally.
| Manufacturer Name | Primary HQ | Key Product Specialization | Min. MOQ Range | Audit & Tech Badges |
|---|---|---|---|---|
| 1. Guangdong NovaFair Fashion Co., Ltd. | Guangdong, China | Custom Athleisure, Heavyweight Hoodies, Cargo Pants, Denim | 2 Pcs (Ultra Flexible) | ISO9001, OEKO-TEX, Rapid Prototyping |
| 2. Shenzhou International Group | Zhejiang, China | High-Volume Knit Activewear, Performance Running Tees | 10,000 Pcs | VERTICALLY INTEGRATED, HIGG, WRAP |
| 3. Eclat Textile Co., Ltd. | Taiwan, China | Engineered Stretch Knits, Seamless Activewear | 3,000 Pcs | BLUESIGN, GRS, Specialized R&D Hub |
| 4. Crystal International Group | Hong Kong, China | Lifestyle Athleisure, Tech Fleece, Circular Denim | 5,000 Pcs | ISO14001, Sustainable Smart Factory |
| 5. Regina Miracle International | Shenzhen, China | Seamless Sports Bras, Bonded Leggings, Molded Apparel | 2,000 Pcs | 3D Mold Patent Holder, Modern R&D |
| 6. Makalot Industrial Co., Ltd. | Taiwan, China | Multi-category Sportswear, Active Outerwear | 3,000 Pcs | Global Multi-Base Operations |
| 7. Youngone Corporation | South Korea | Technical Outdoor Gear, Bonded Performance Apparel | 5,000 Pcs | GORE-TEX Certified, Enterprise OEM |
| 8. Hansae Co., Ltd. | South Korea | Mass Market Casual Wear, Athletic Basics | 10,000 Pcs | Lean Automation, High Output |
| 9. TAL Apparel | Hong Kong, China | Technical Smart Apparel, Wrinkle-Free Casual Athleisure | 3,000 Pcs | Inno-Tailoring Patents, Custom Logistics |
| 10. Yue Yuen Industrial | Hong Kong, China | Athletic Footwear & Integrated Performance Wear | 10,000 Pcs | Global Tier-1 Brand Partner |
Competitive Advantage: Exceptional agility, zero-friction client onboarding, and deep customization capabilities. With over two decades of technical garment expertise, NovaFair bridges the gap between boutique fashion design and large-scale industrial manufacturing. Their industry-disrupting Low MOQ (from 2 pieces) allows emerging D2C brands, streetwear labels, and corporate enterprises to test specialized collections without massive capital lockup. Fully outfitted with laser cutters, automated pattern equipment, and multi-technique printing systems (puff, screen, thermal transfer).
Competitive Advantage: Industrial scale and total vertical integration. Handling every phase from yarn spinning, weaving, dyeing, and finishing to cut-and-sew, Shenzhou is the powerhouse supplier behind global athletic titans. Their massive manufacturing ecosystem provides unmatched volume economies, though access is generally restricted to Fortune 500 orders requiring high minimum quantities.
Competitive Advantage: Fabric-first technical innovation. Eclat is globally renowned for its proprietary knit technology, developing specialized synthetic textiles featuring superior elongation, recovery, and moisture control. Their dedicated R&D lab continually sets benchmark standards for premium activewear leggings and high-performance base layers.
Competitive Advantage: Eco-efficiency and digital manufacturing. Operating digital smart factories across Asia, Crystal International excels in large-scale lifestyle athleisure, incorporating recycled cotton-poly blends and waterless garment dyeing technologies for eco-conscious global retailers.
Competitive Advantage: 3D molding, bonding, and seamless engineering. Capitalizing on deep expertise in structural lingerie engineering, Regina Miracle revolutionized the sports bra and seamless legging sector through patented 3D foam molding and stitchless ultrasonic bonding technology.
Competitive Advantage: Cross-category versatility and smart analytics. Makalot provides end-to-end supply chain integration across activewear, casual wear, and outerwear, leveraging real-time inventory and market trend algorithms to optimize customer production planning.
For global apparel procurement directors and brand owners, selecting an activewear manufacturing partner requires evaluating operational risk metrics beyond FOB price per unit. Below is the standard 4-Pillar Verification Blueprint used by top-tier apparel auditors:
Verify mill lab certifications for fabric weight (GSM consistency ±3%), Dimensional Stability after Washing (AATCC 135), Color Fastness to Rubbing (ISO 105-X12), and Four-Way Stretch Recovery percentage.
Inspect flatlock seam tension (6-needle 4-thread), seam burst strength, thread breaking limits under maximum stretch, and thermal tape adhesion durability through repeated wash cycles.
Ensure vendor compliance with international social audits (BSCI, WRAP), chemical traceability (REACH compliance), and environmental fabric standards (OEKO-TEX Standard 100, GRS).
Calculate true land-to-warehouse costs by factoring in sampling lead times, defect allowance thresholds (AQL 1.5 vs 2.5), tariff optimization, and low-MOQ inventory liquidity advantages.
Different brand models present distinct manufacturing challenges. A customized OEM/ODM solution must align with your specific commercial model:
Challenge: Rapid style iterations, unpredictable demand forecasting, and inventory risk.
Solution: Leverage agile suppliers like Guangdong NovaFair. Utilize low MOQ starting at 2-50 pieces to launch micro-capsules, gauge market response via D2C ads, and trigger rapid-scale replenishment orders within 14 days.
Challenge: Blending athletic functionality with heavy-weight aesthetic cottons, customized distressing, puff printing, and precise vintage garment washes.
Solution: Specialized hybrid manufacturing line combining heavy French Terry (400-500 GSM), custom rhinestone embellishments, 3D foam prints, and vintage acid wash treatments.
Challenge: Tight delivery timelines, strict color consistency across multiple SKUs, and durable high-frequency wash resistance.
Solution: Standardized stock-blank custom program with automated silicone heat-transfer branding, rapid sublimation printing, and batch-to-batch color matching guarantee.
For custom tech packs, sample creation (including digital pattern grading and initial physical prototype) typically takes 5 to 7 business days. Once tech pack and fit samples are approved, bulk production turnaround spans 15 to 25 calendar days, depending on fabric custom dyeing requirements and total order quantity.
NovaFair maintains a vast in-stock inventory of premium performance fabrics (such as 280-500 GSM heavy cottons, nylon-spandex 4-way stretch, and technical polyester fleeces). Combined with digital CAD cutting beds and versatile single-line sewing cells, we eliminate setup inefficiencies, allowing us to serve emerging designers and boutique test runs at ultra-low quantities.
For high-compression active leggings, an optimal blend is 75-80% Nylon with 20-25% Elastane at a weight of 220–260 GSM for opacity ("squat-proof") and breathability. For streetwear athleisure hoodies, heavy 100% Cotton French Terry or Cotton-Poly fleece at 400 to 500 GSM offers the structured drop-shoulder silhouette sought in modern urban fashion.
A robust Quality Assurance workflow follows the AQL 1.5 standard across four inspection checkpoints: 1) Raw Fabric Inspection (4-point system checking GSM, color fastness, shade lot matching), 2) In-Line Sewing Check (stitch tension, measurement drift), 3) Post-Ironing Inspection (seam flatlock integrity), and 4) Final Pre-Packing QC (metal detection, trim check, packing compliance).
Yes. Complete ODM customization includes custom-dyed matching ribbing, engraved metal aglets/zipper pulls, high-density 3D puff print logos, reflective thermal transfers, woven neck labels, recycled polybags, and custom barcode hangtags tailored for international retail fulfillment.
Browse our additional high-demand catalog items including windbreakers, heavy French Terry hoodies, outdoor trekking pants, and quick-dry athletic wear engineered for international distribution.



 NovaFair Fashion